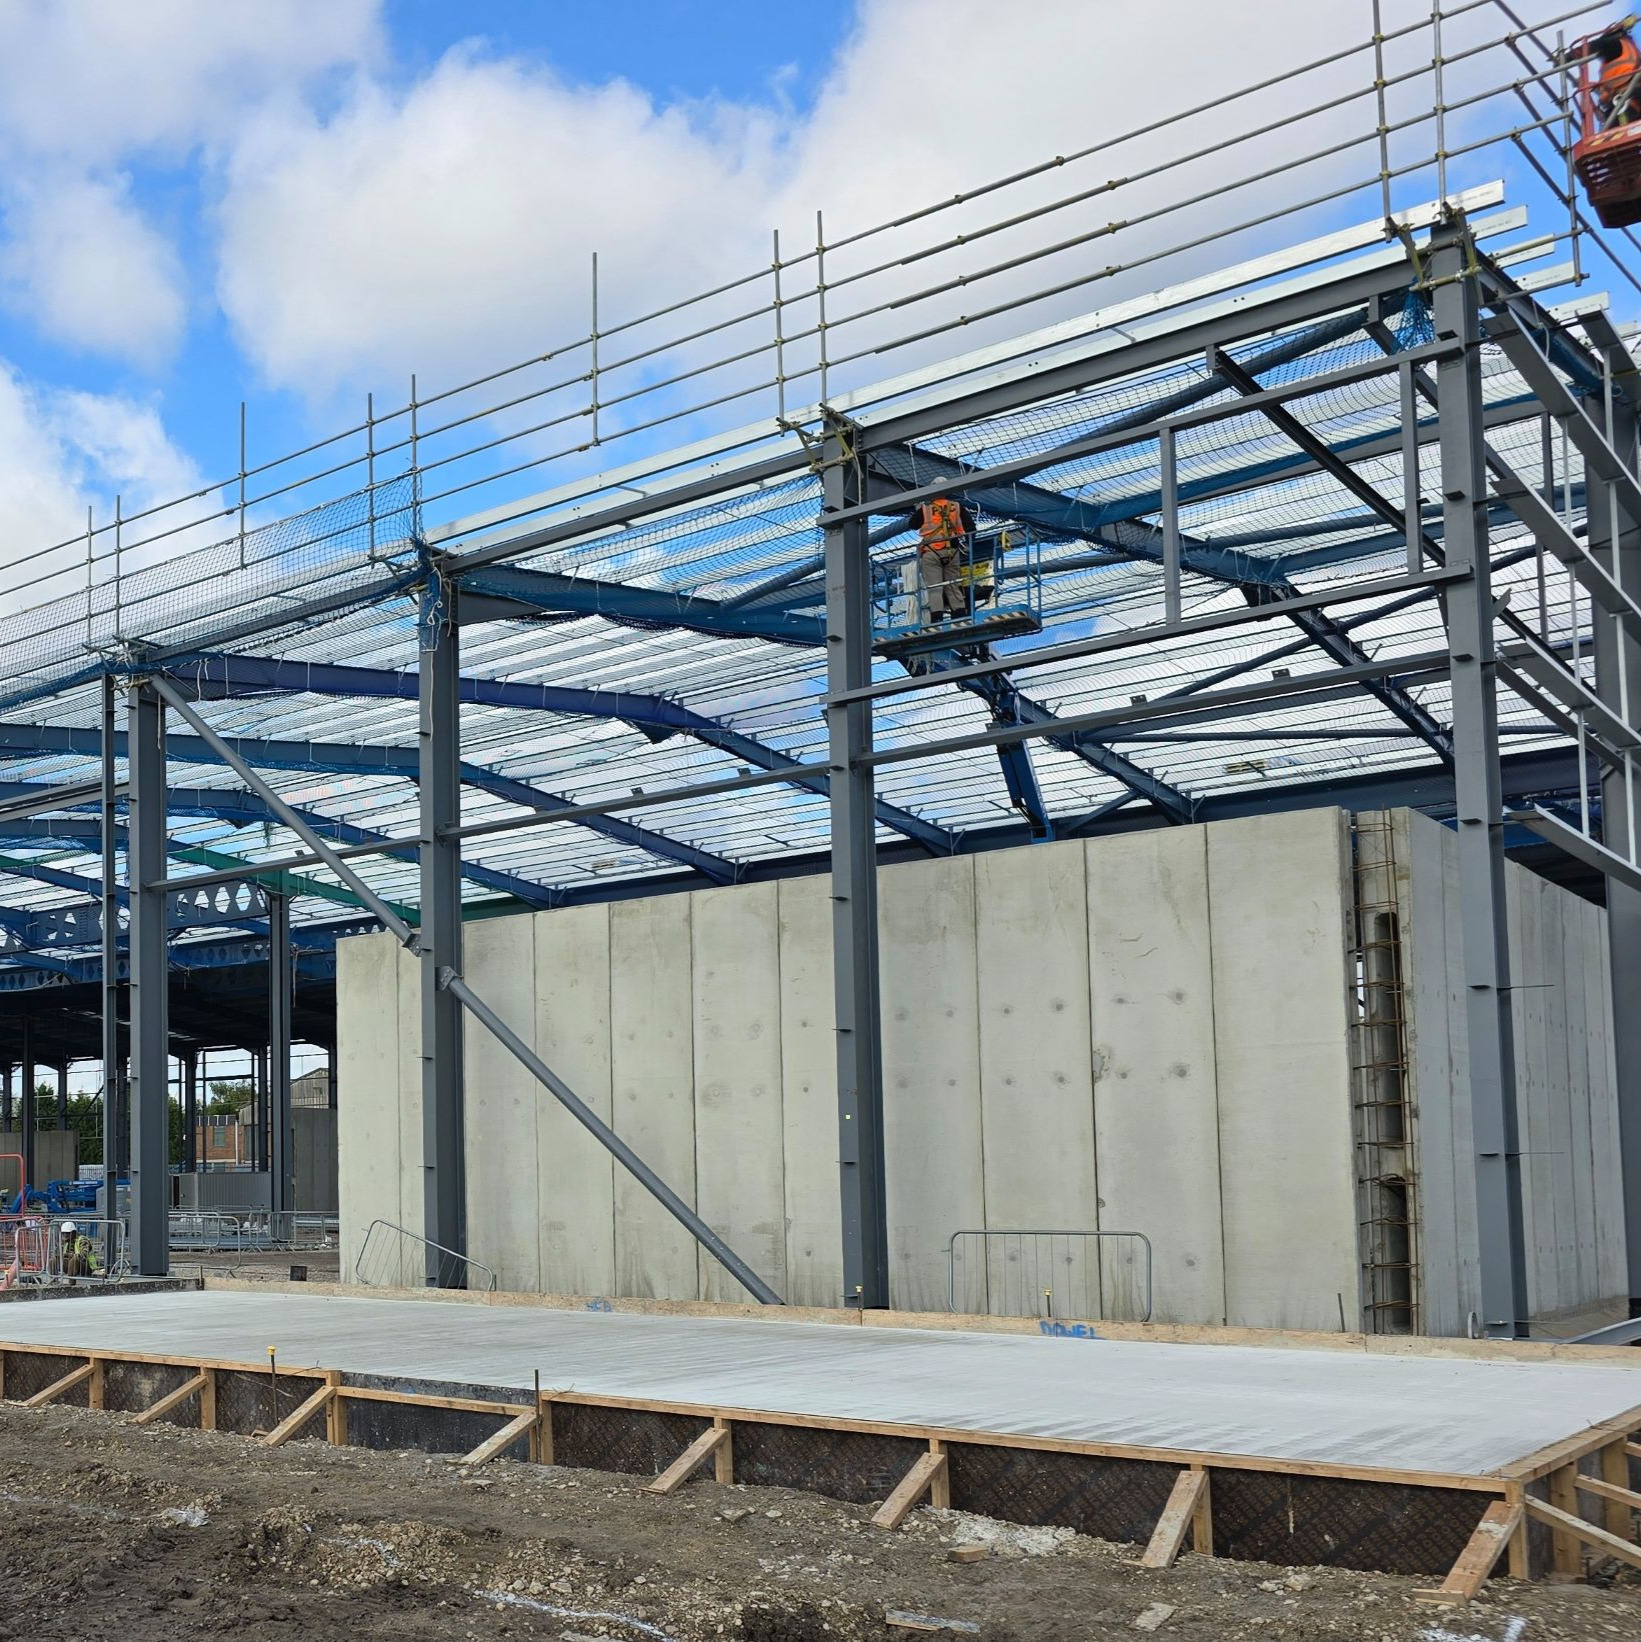
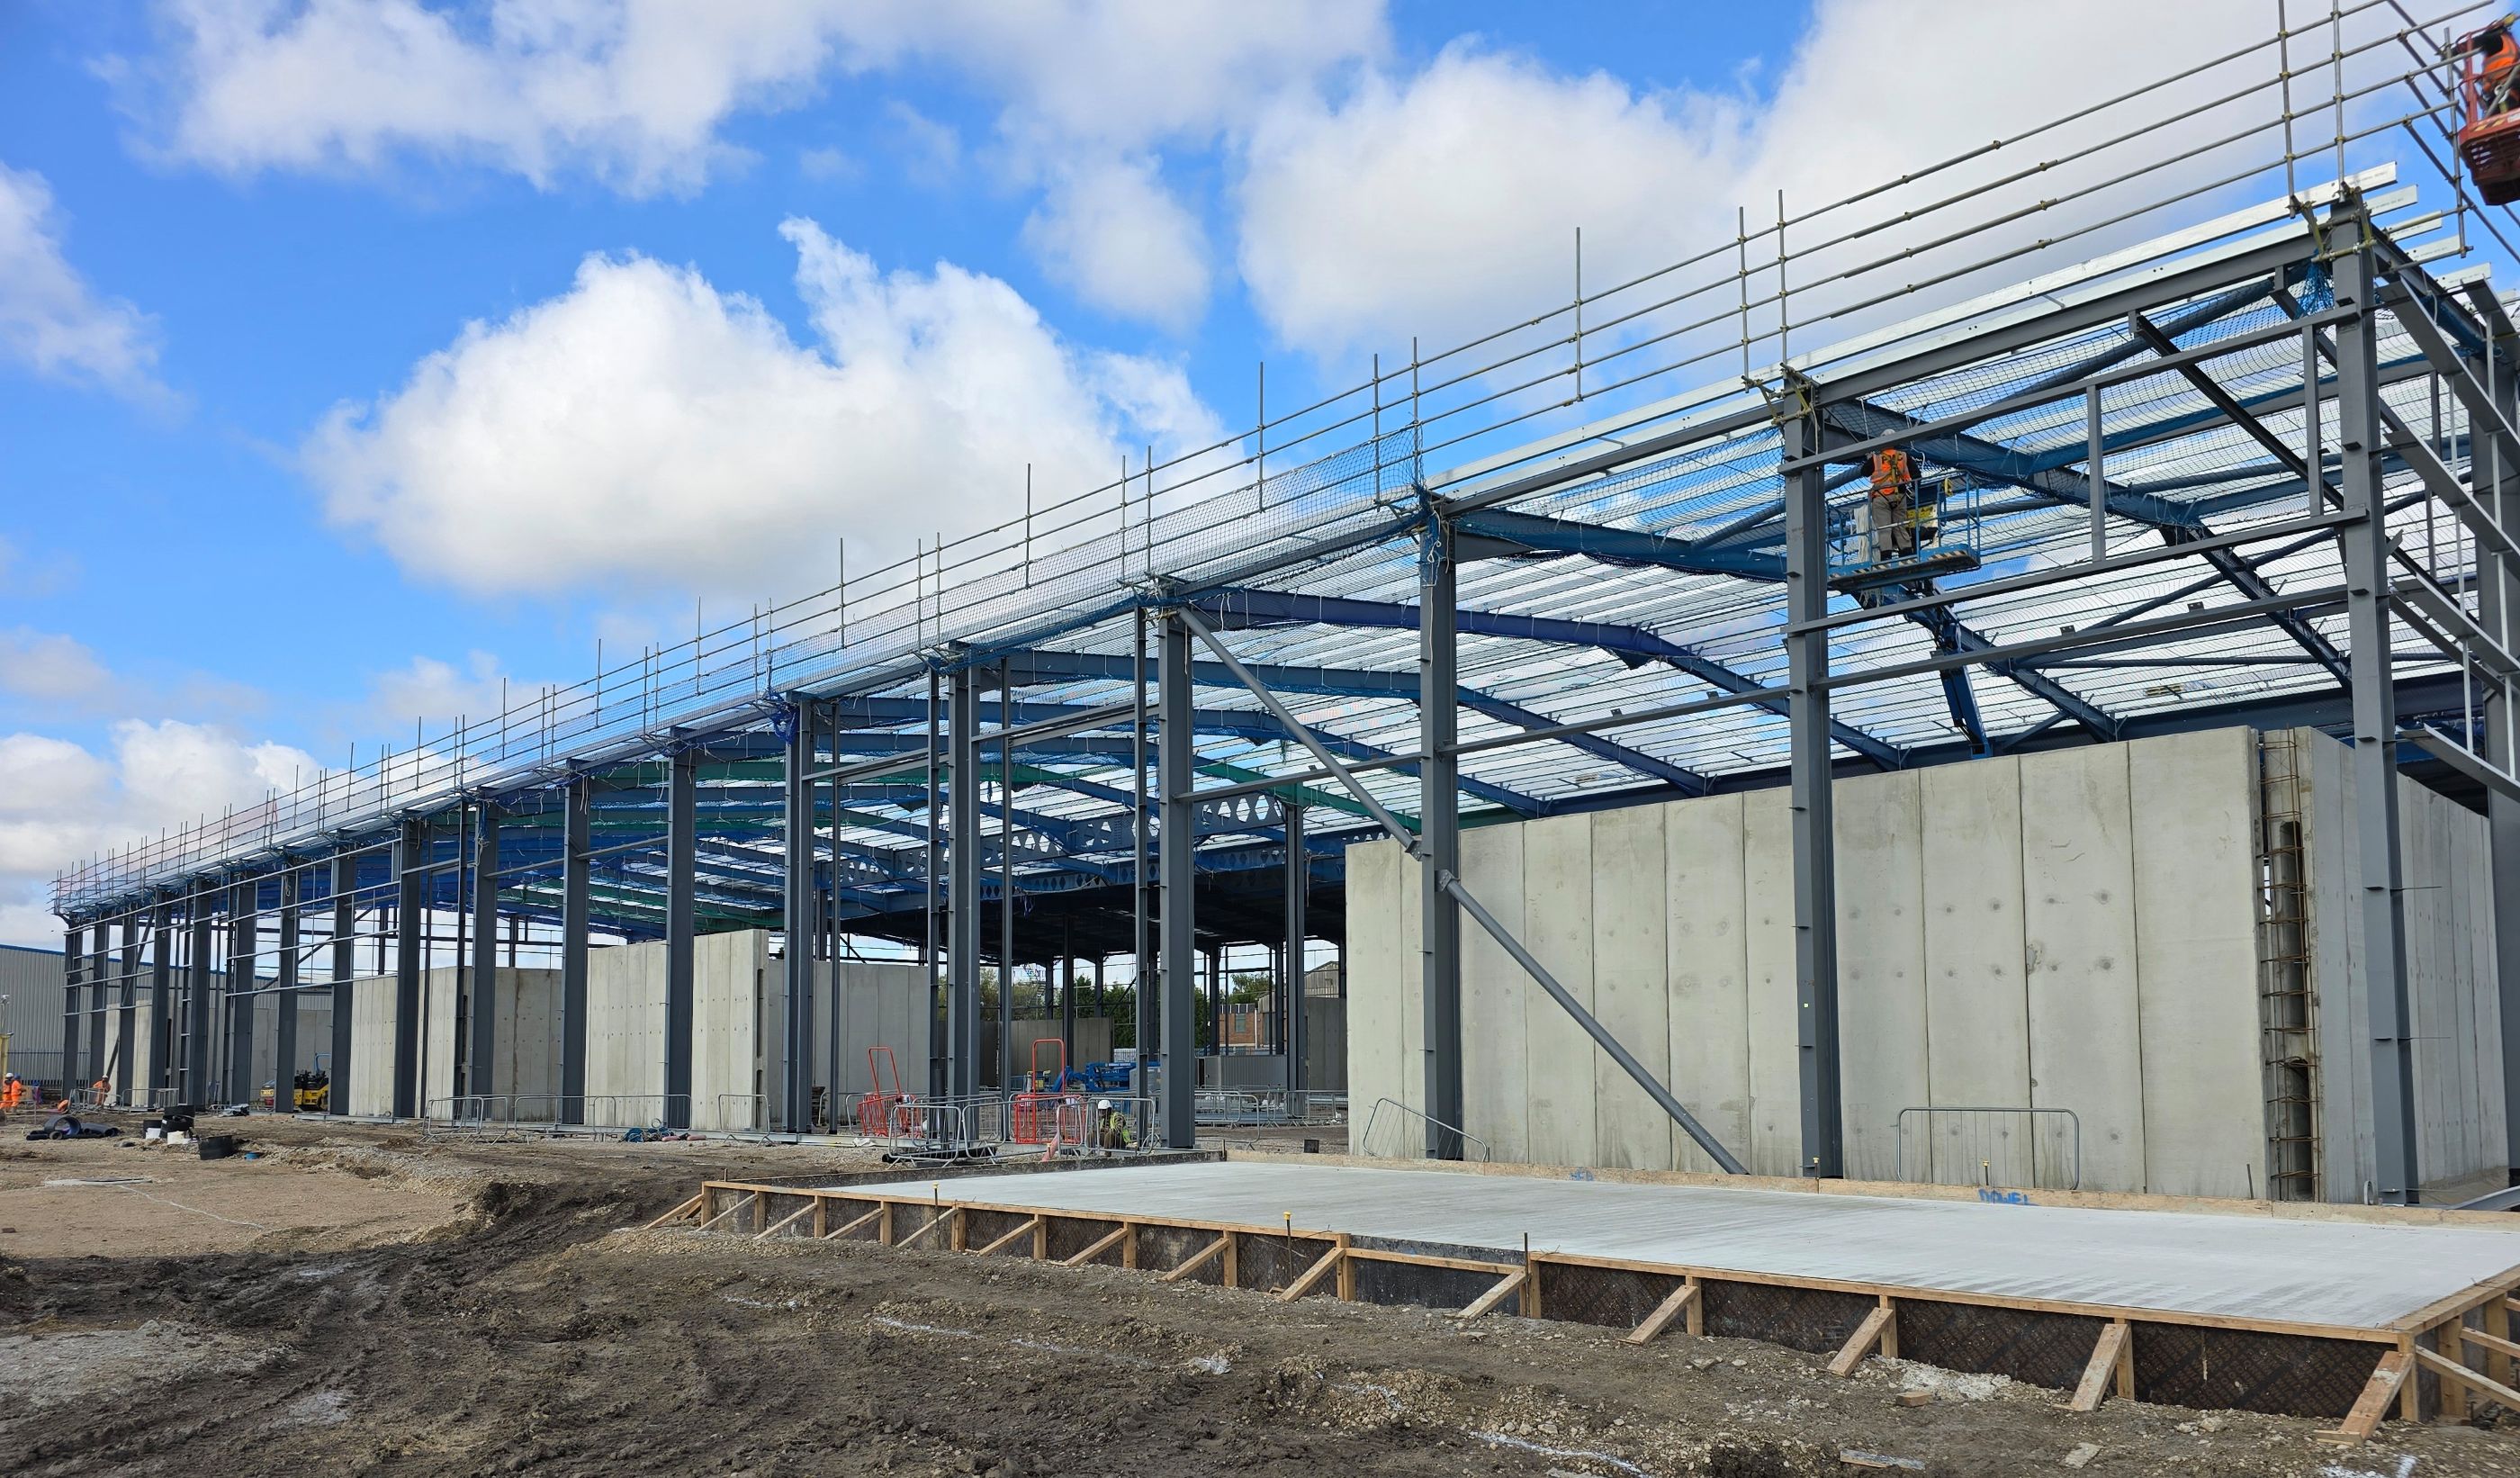
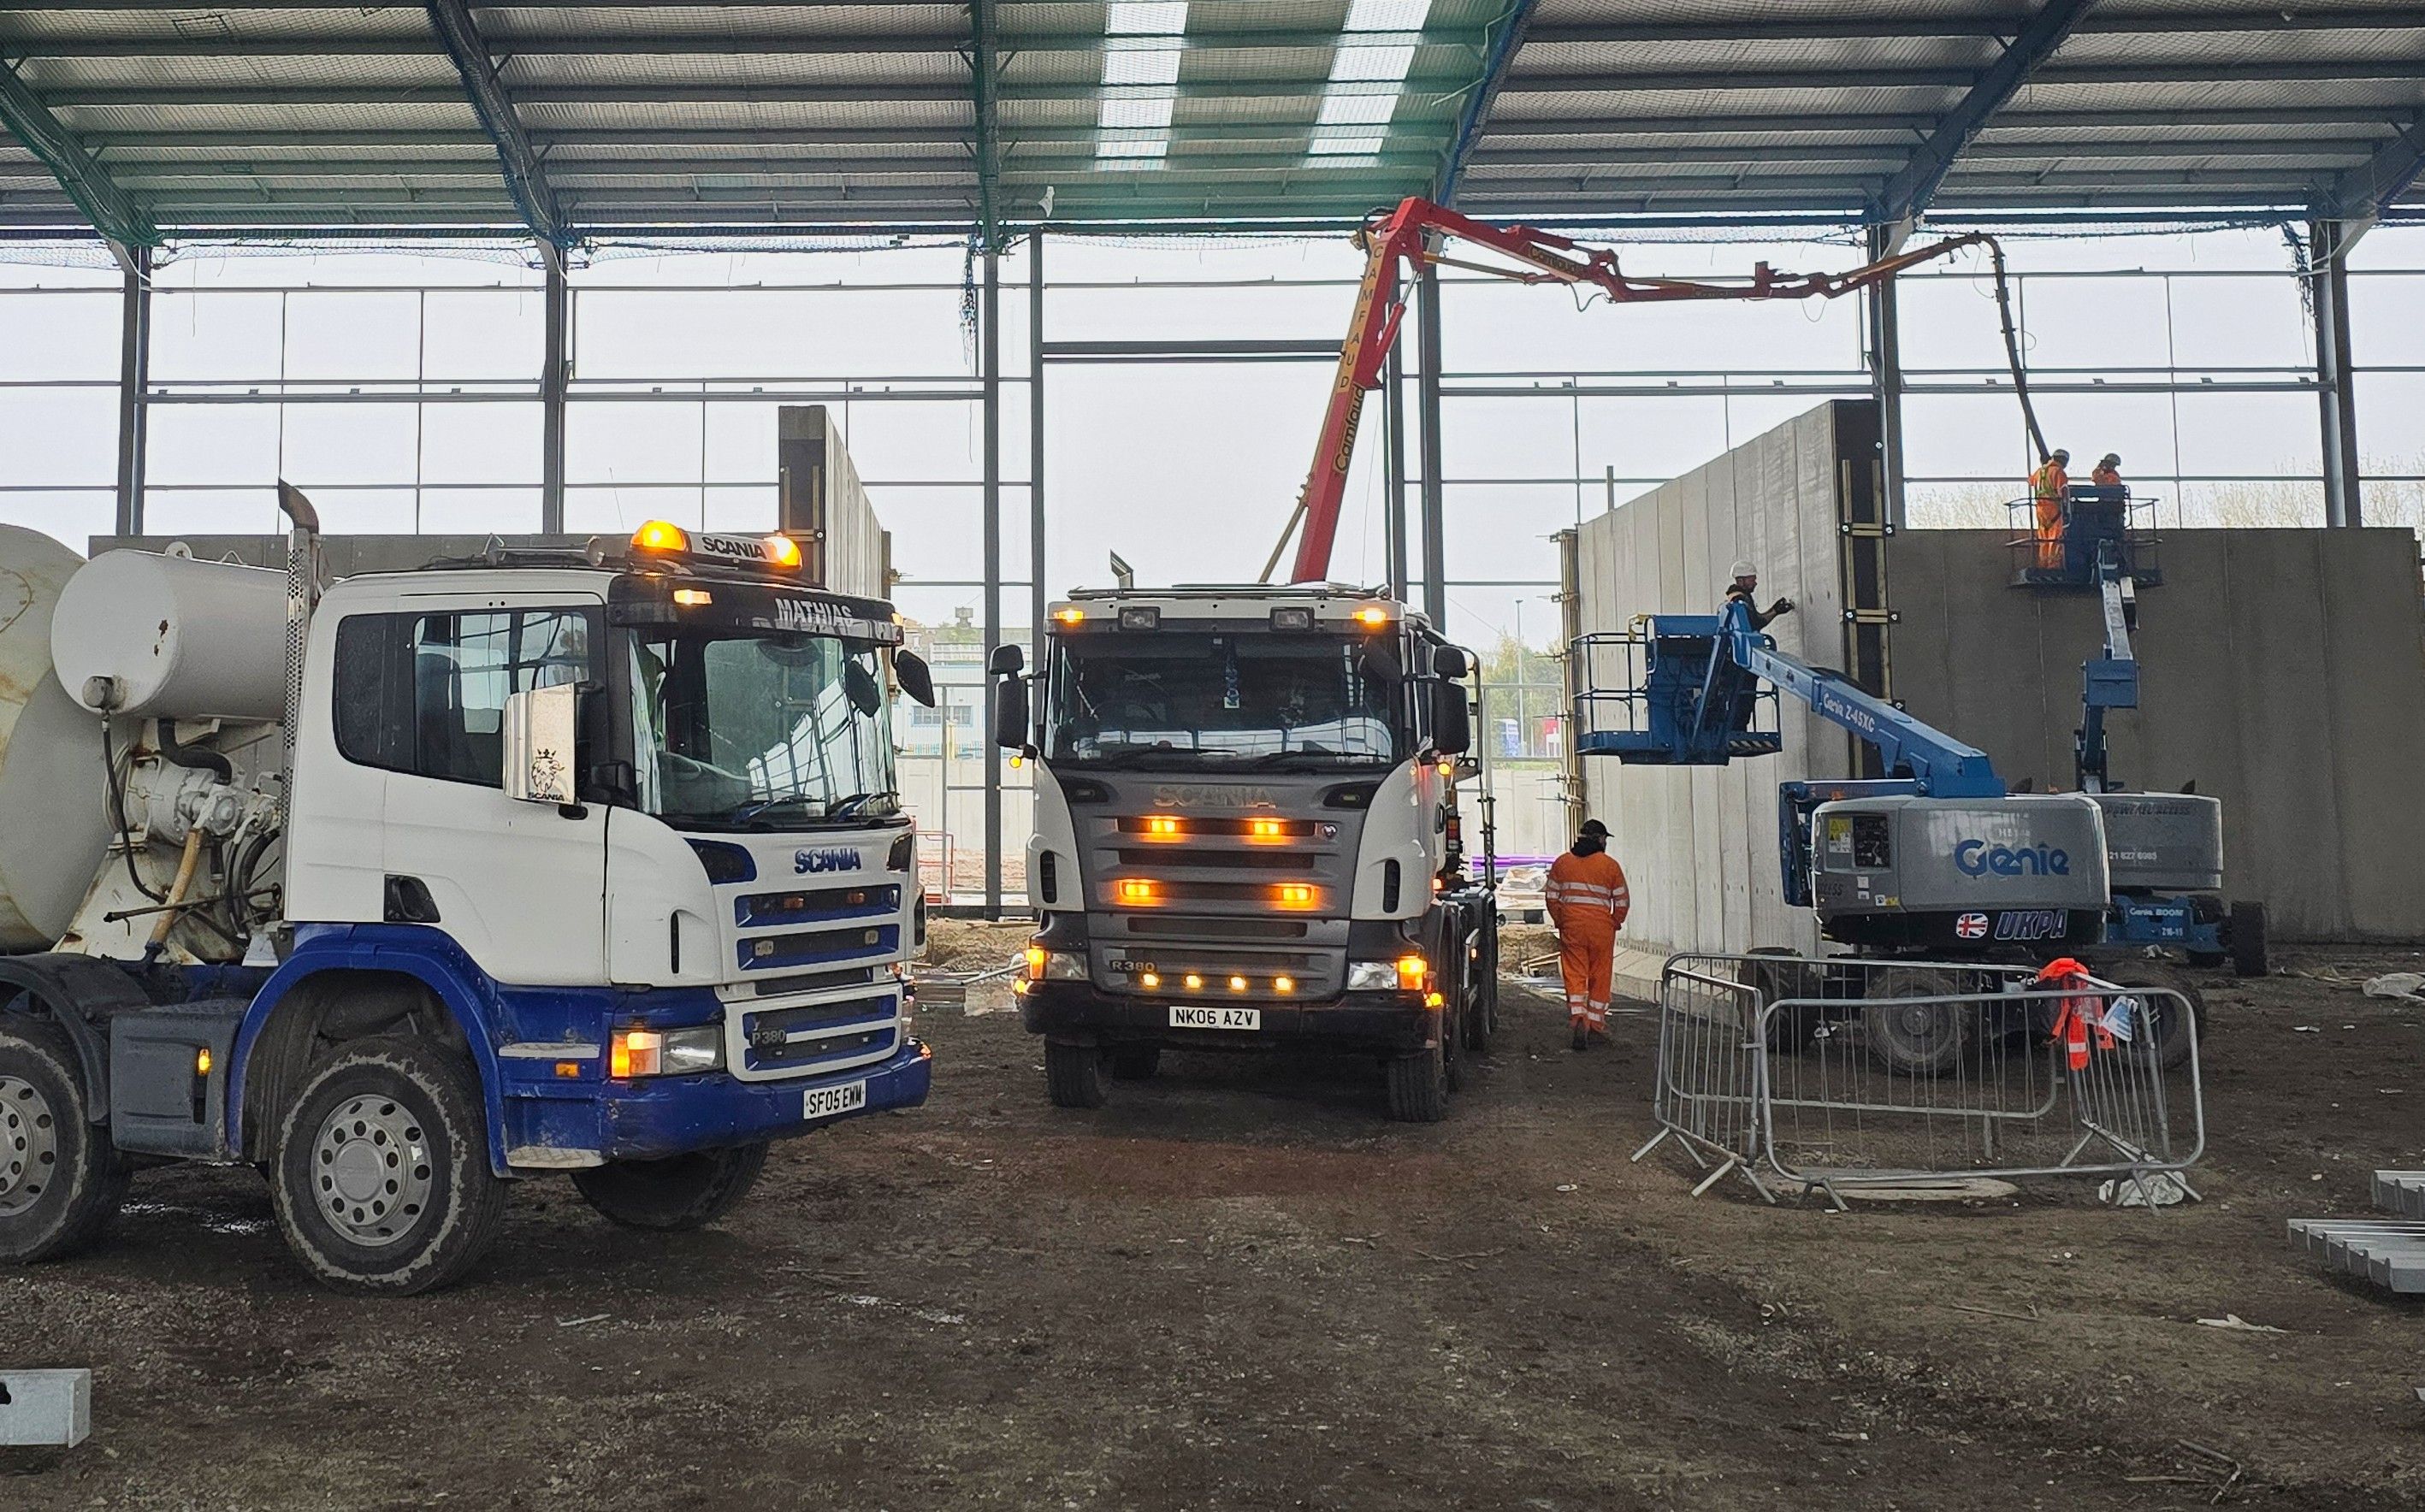
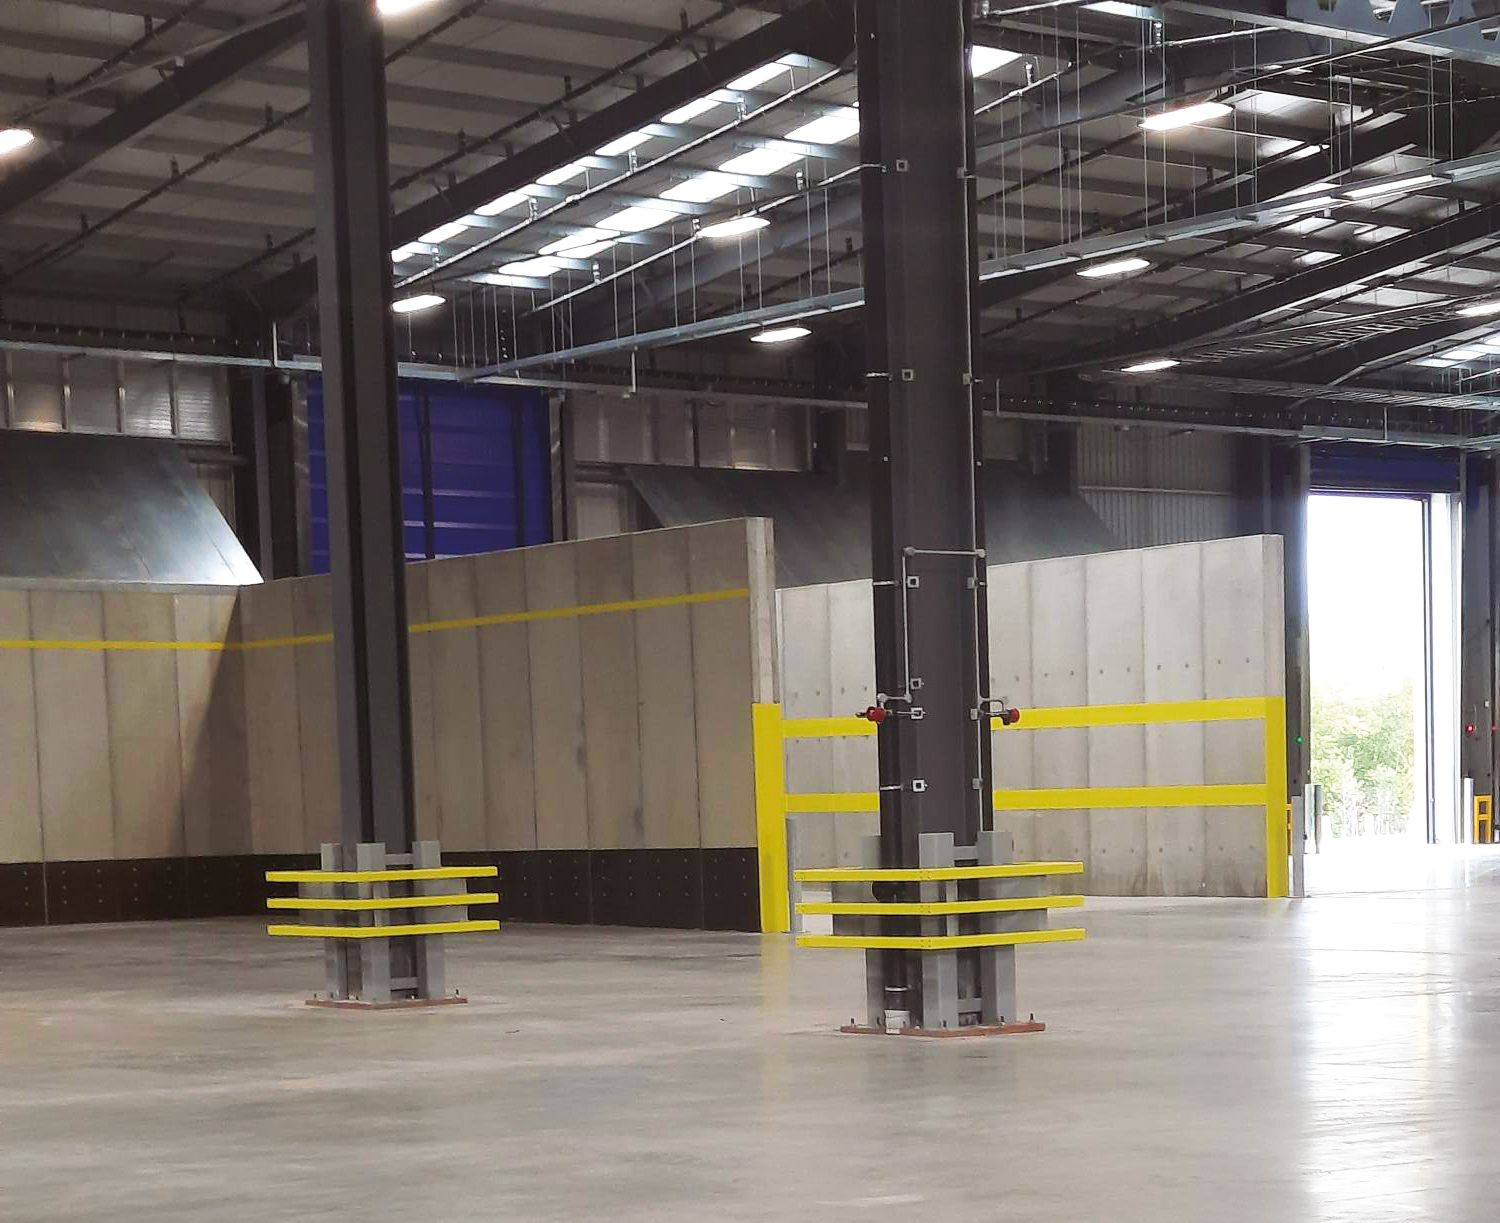
A brand new recycling centre capable of handling 40,000 tonnes of waste each year has opened on a former brownfield site in the heart of Walsall.
The facility has been created on six hectares of previously waterlogged land at Middlemore Lane. Thought to be Europe’s largest household waste recycling centre, it boasts 19 bays, each housing two skips, allowing residents to recycle everything from electrical items and batteries to household chemicals, oils, textiles and glass. A reuse shop has also been created on site as well as a waste transfer station, where waste is sorted and prepared for onward transport to recycling and disposal facilities.
The £32m project was funded by Walsall Council as part of its long-term strategy to divert waste away from landfill and create a cleaner and greener borough. Morgan Sindall Construction was contracted to engineer and deliver the state-of-the-art scheme and associated infrastructure, including weighbridges, service yards and ventilation systems.
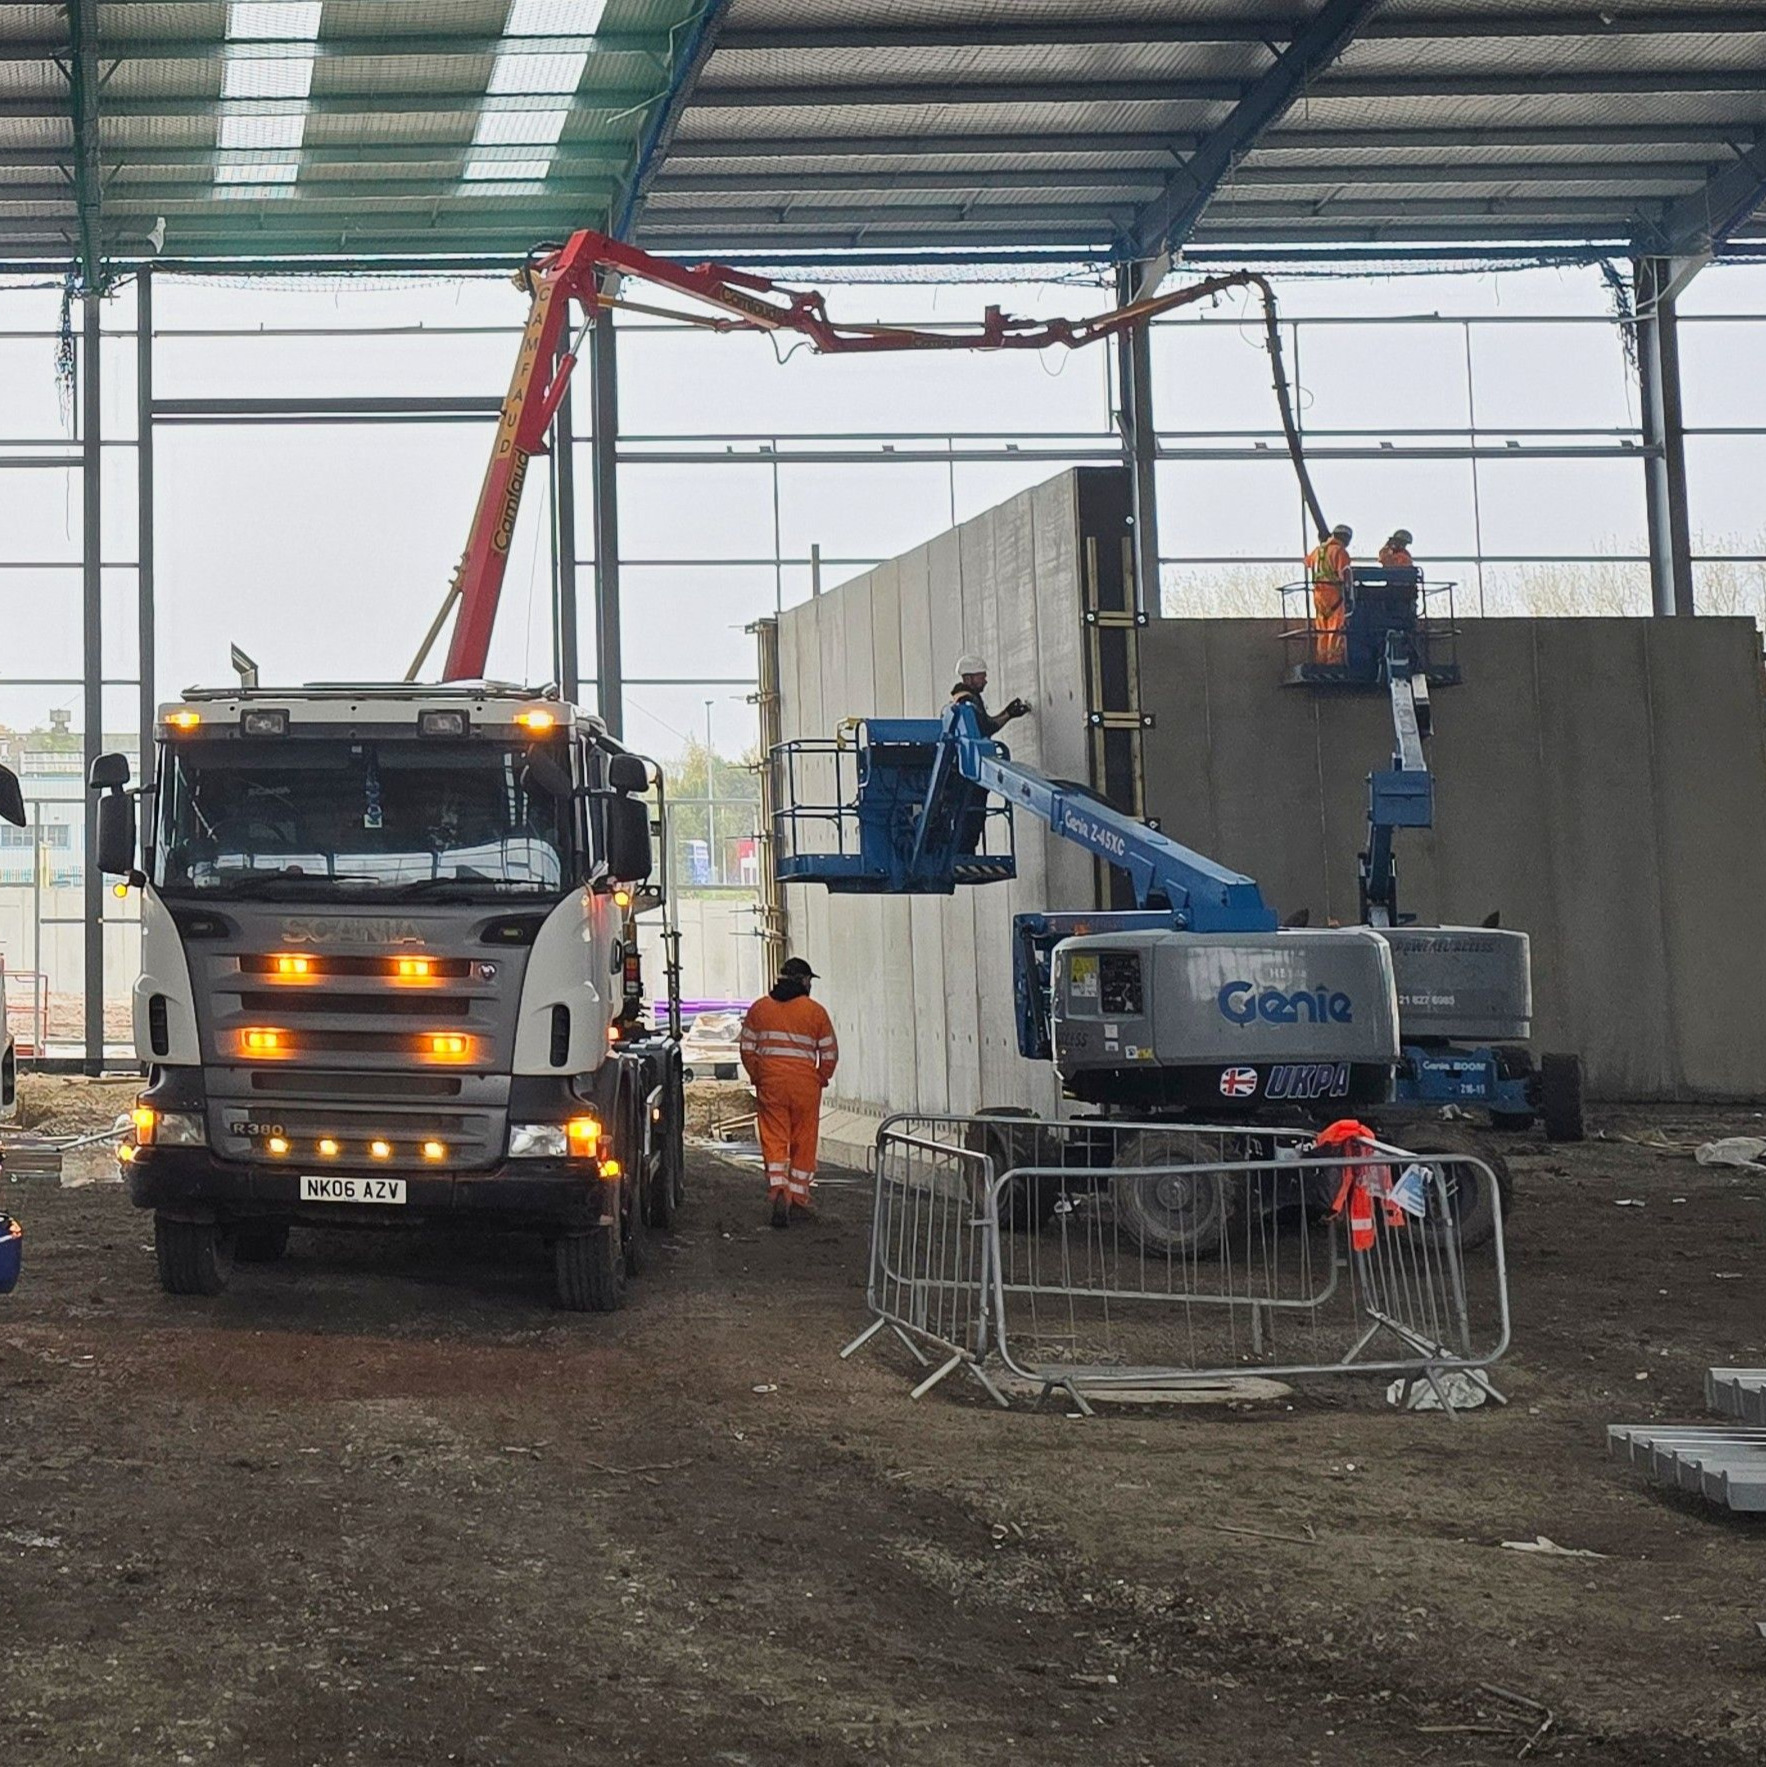
Poundfield Precast played a key role by supplying and installing its robust retaining wall systems to support the construction of this major facility.
Making best use of precast retaining walls
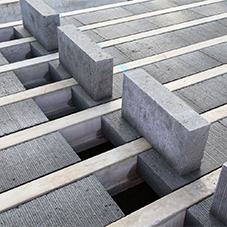
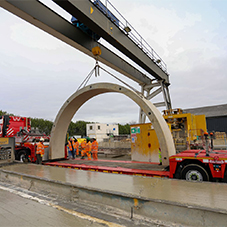
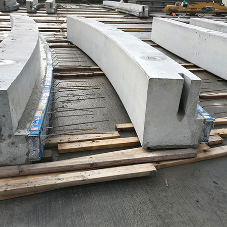
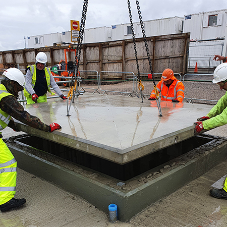
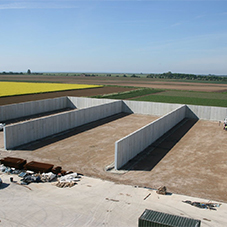
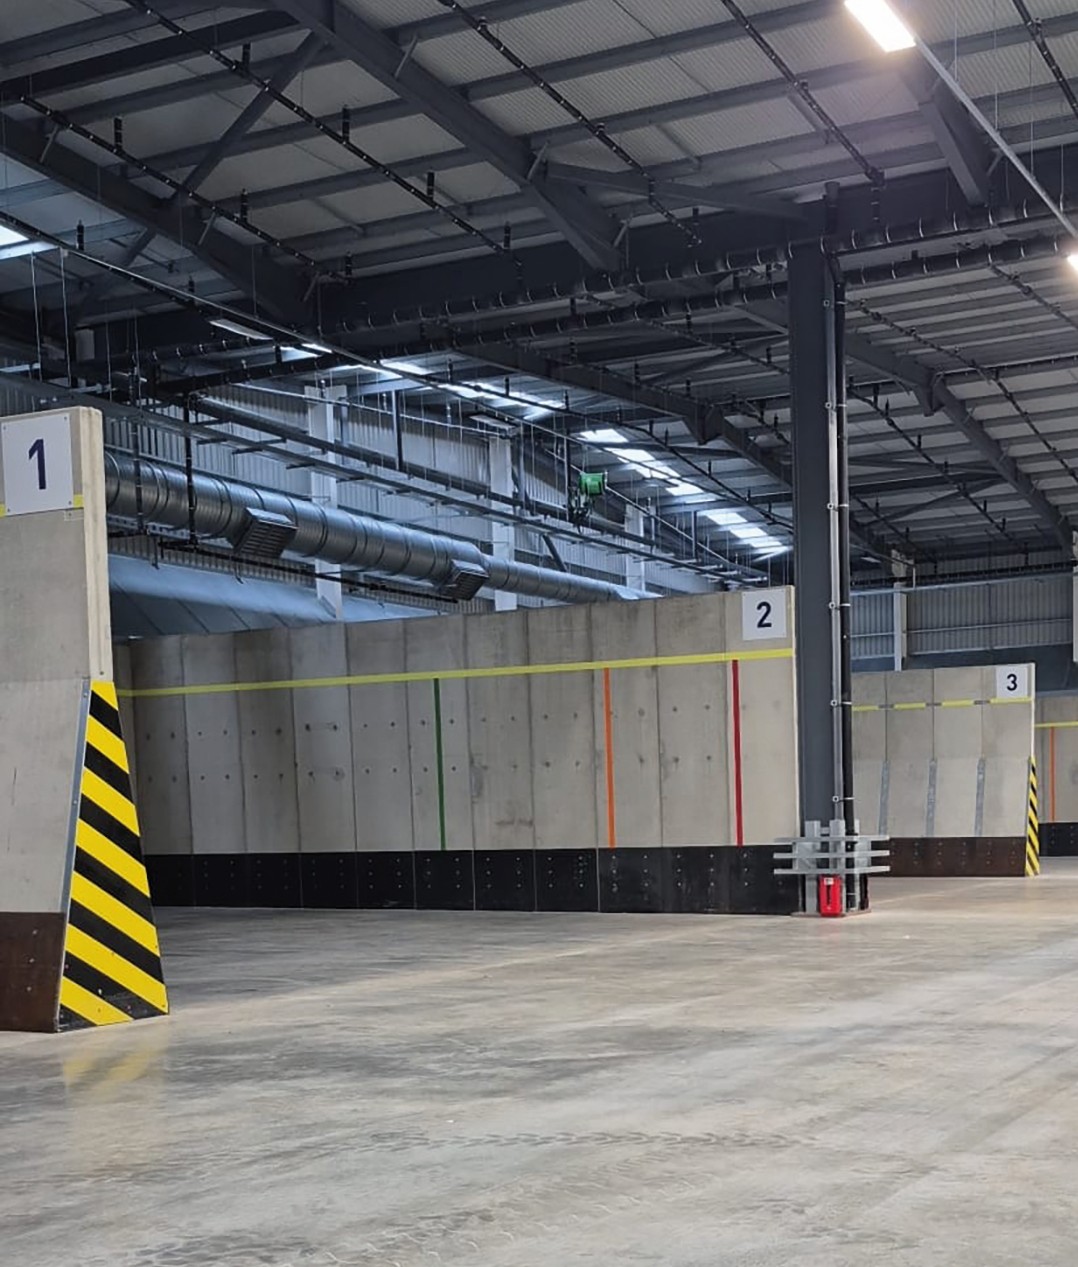
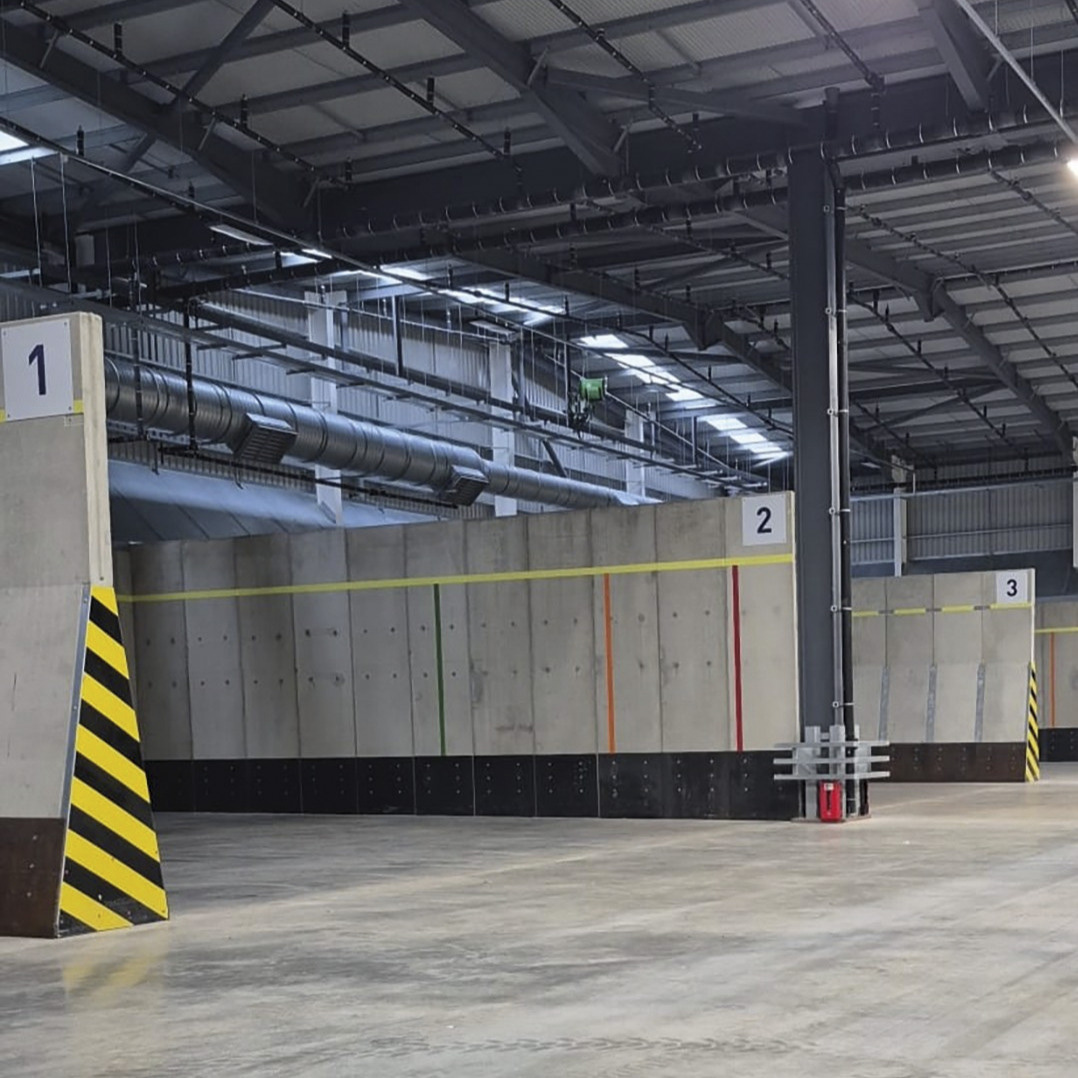
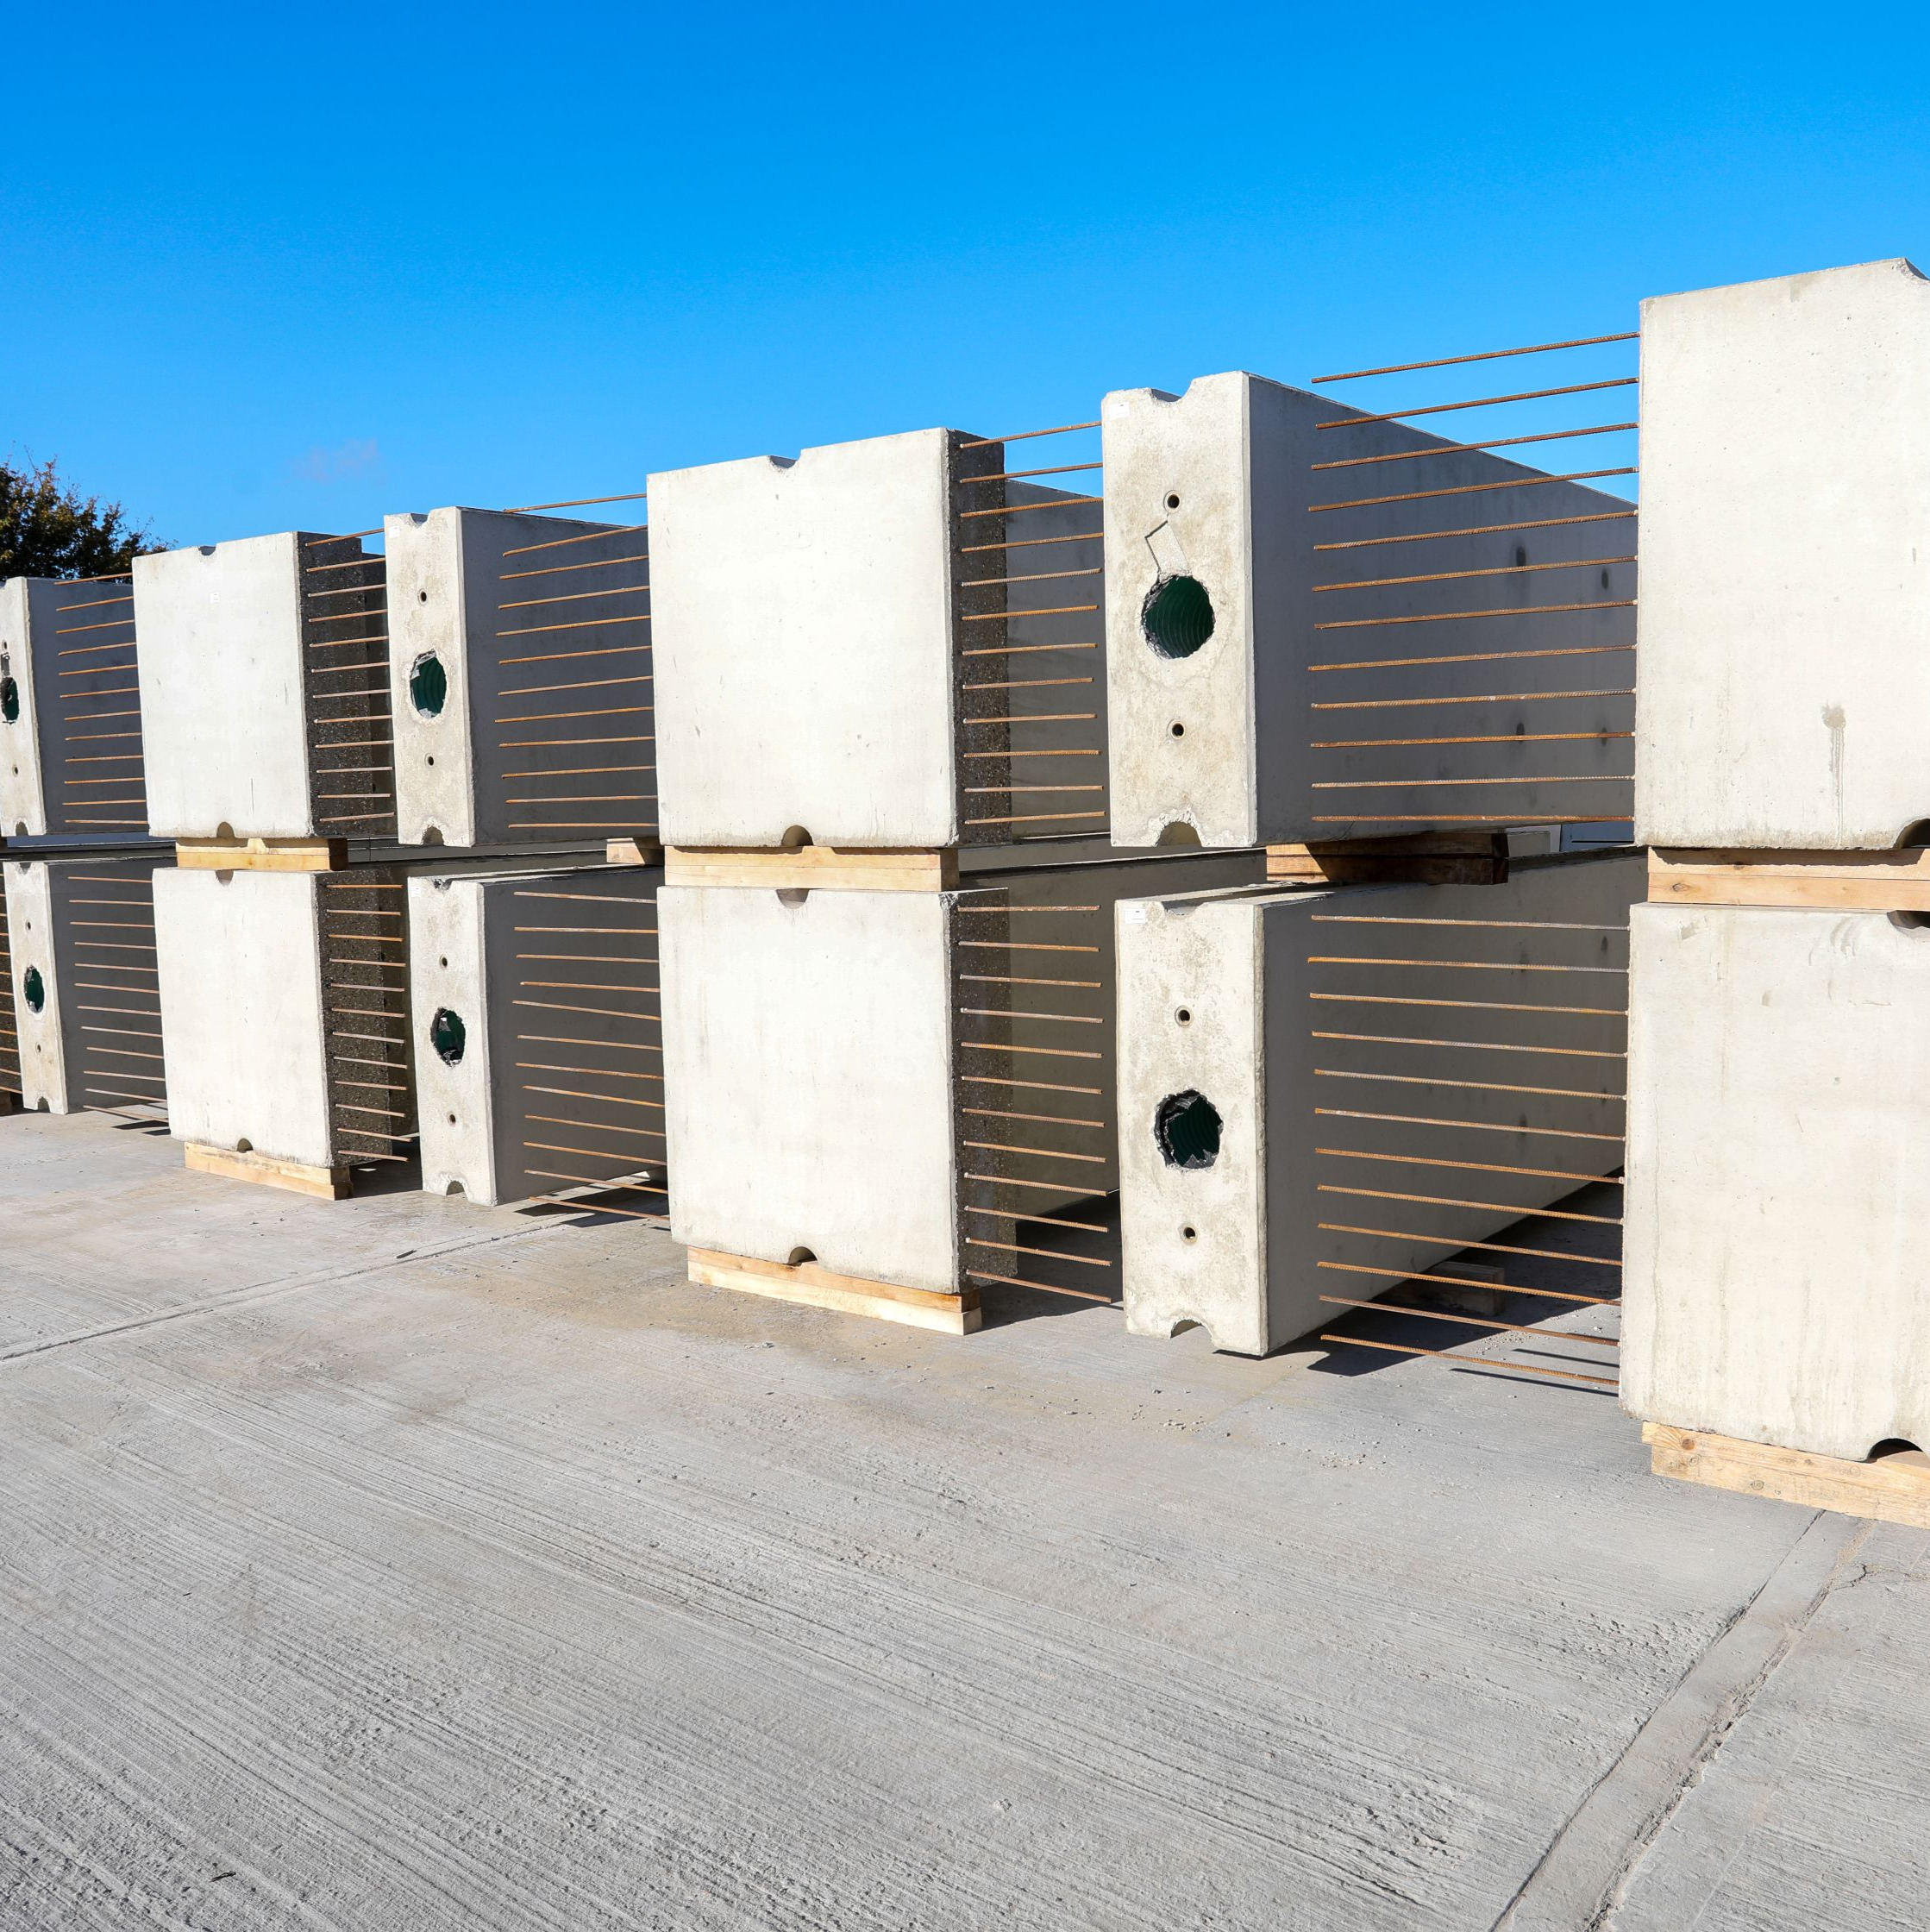
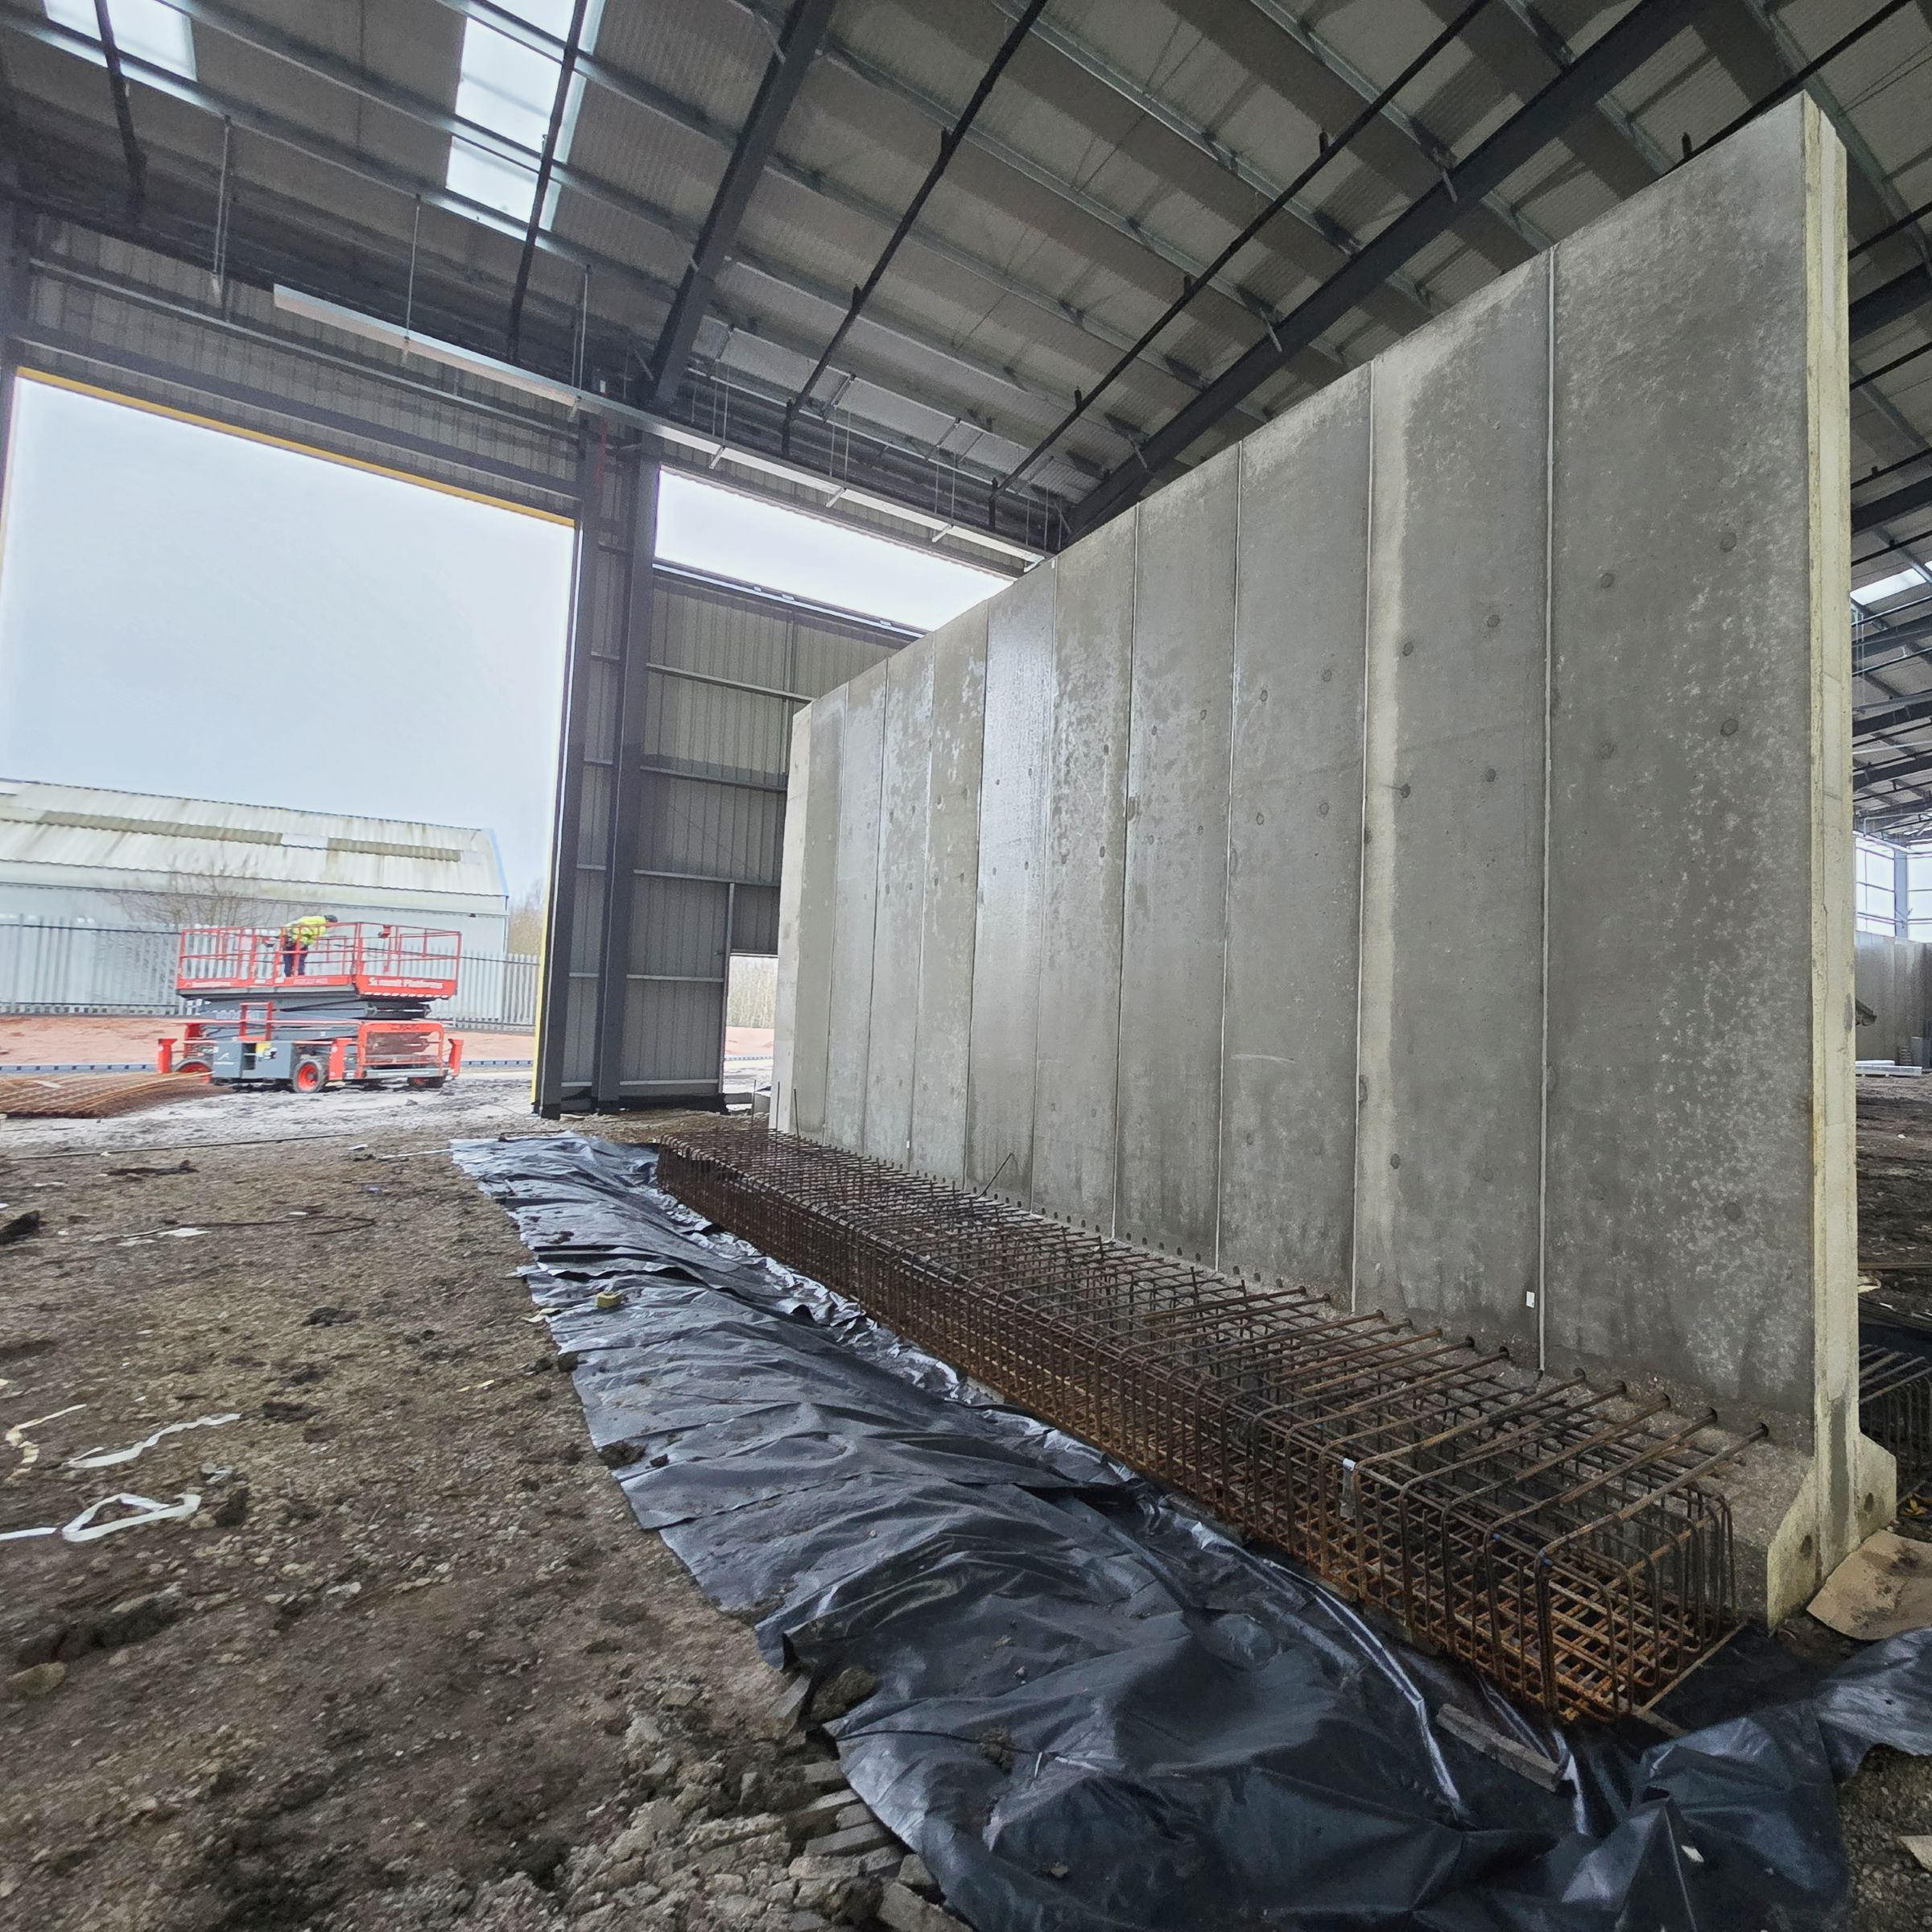
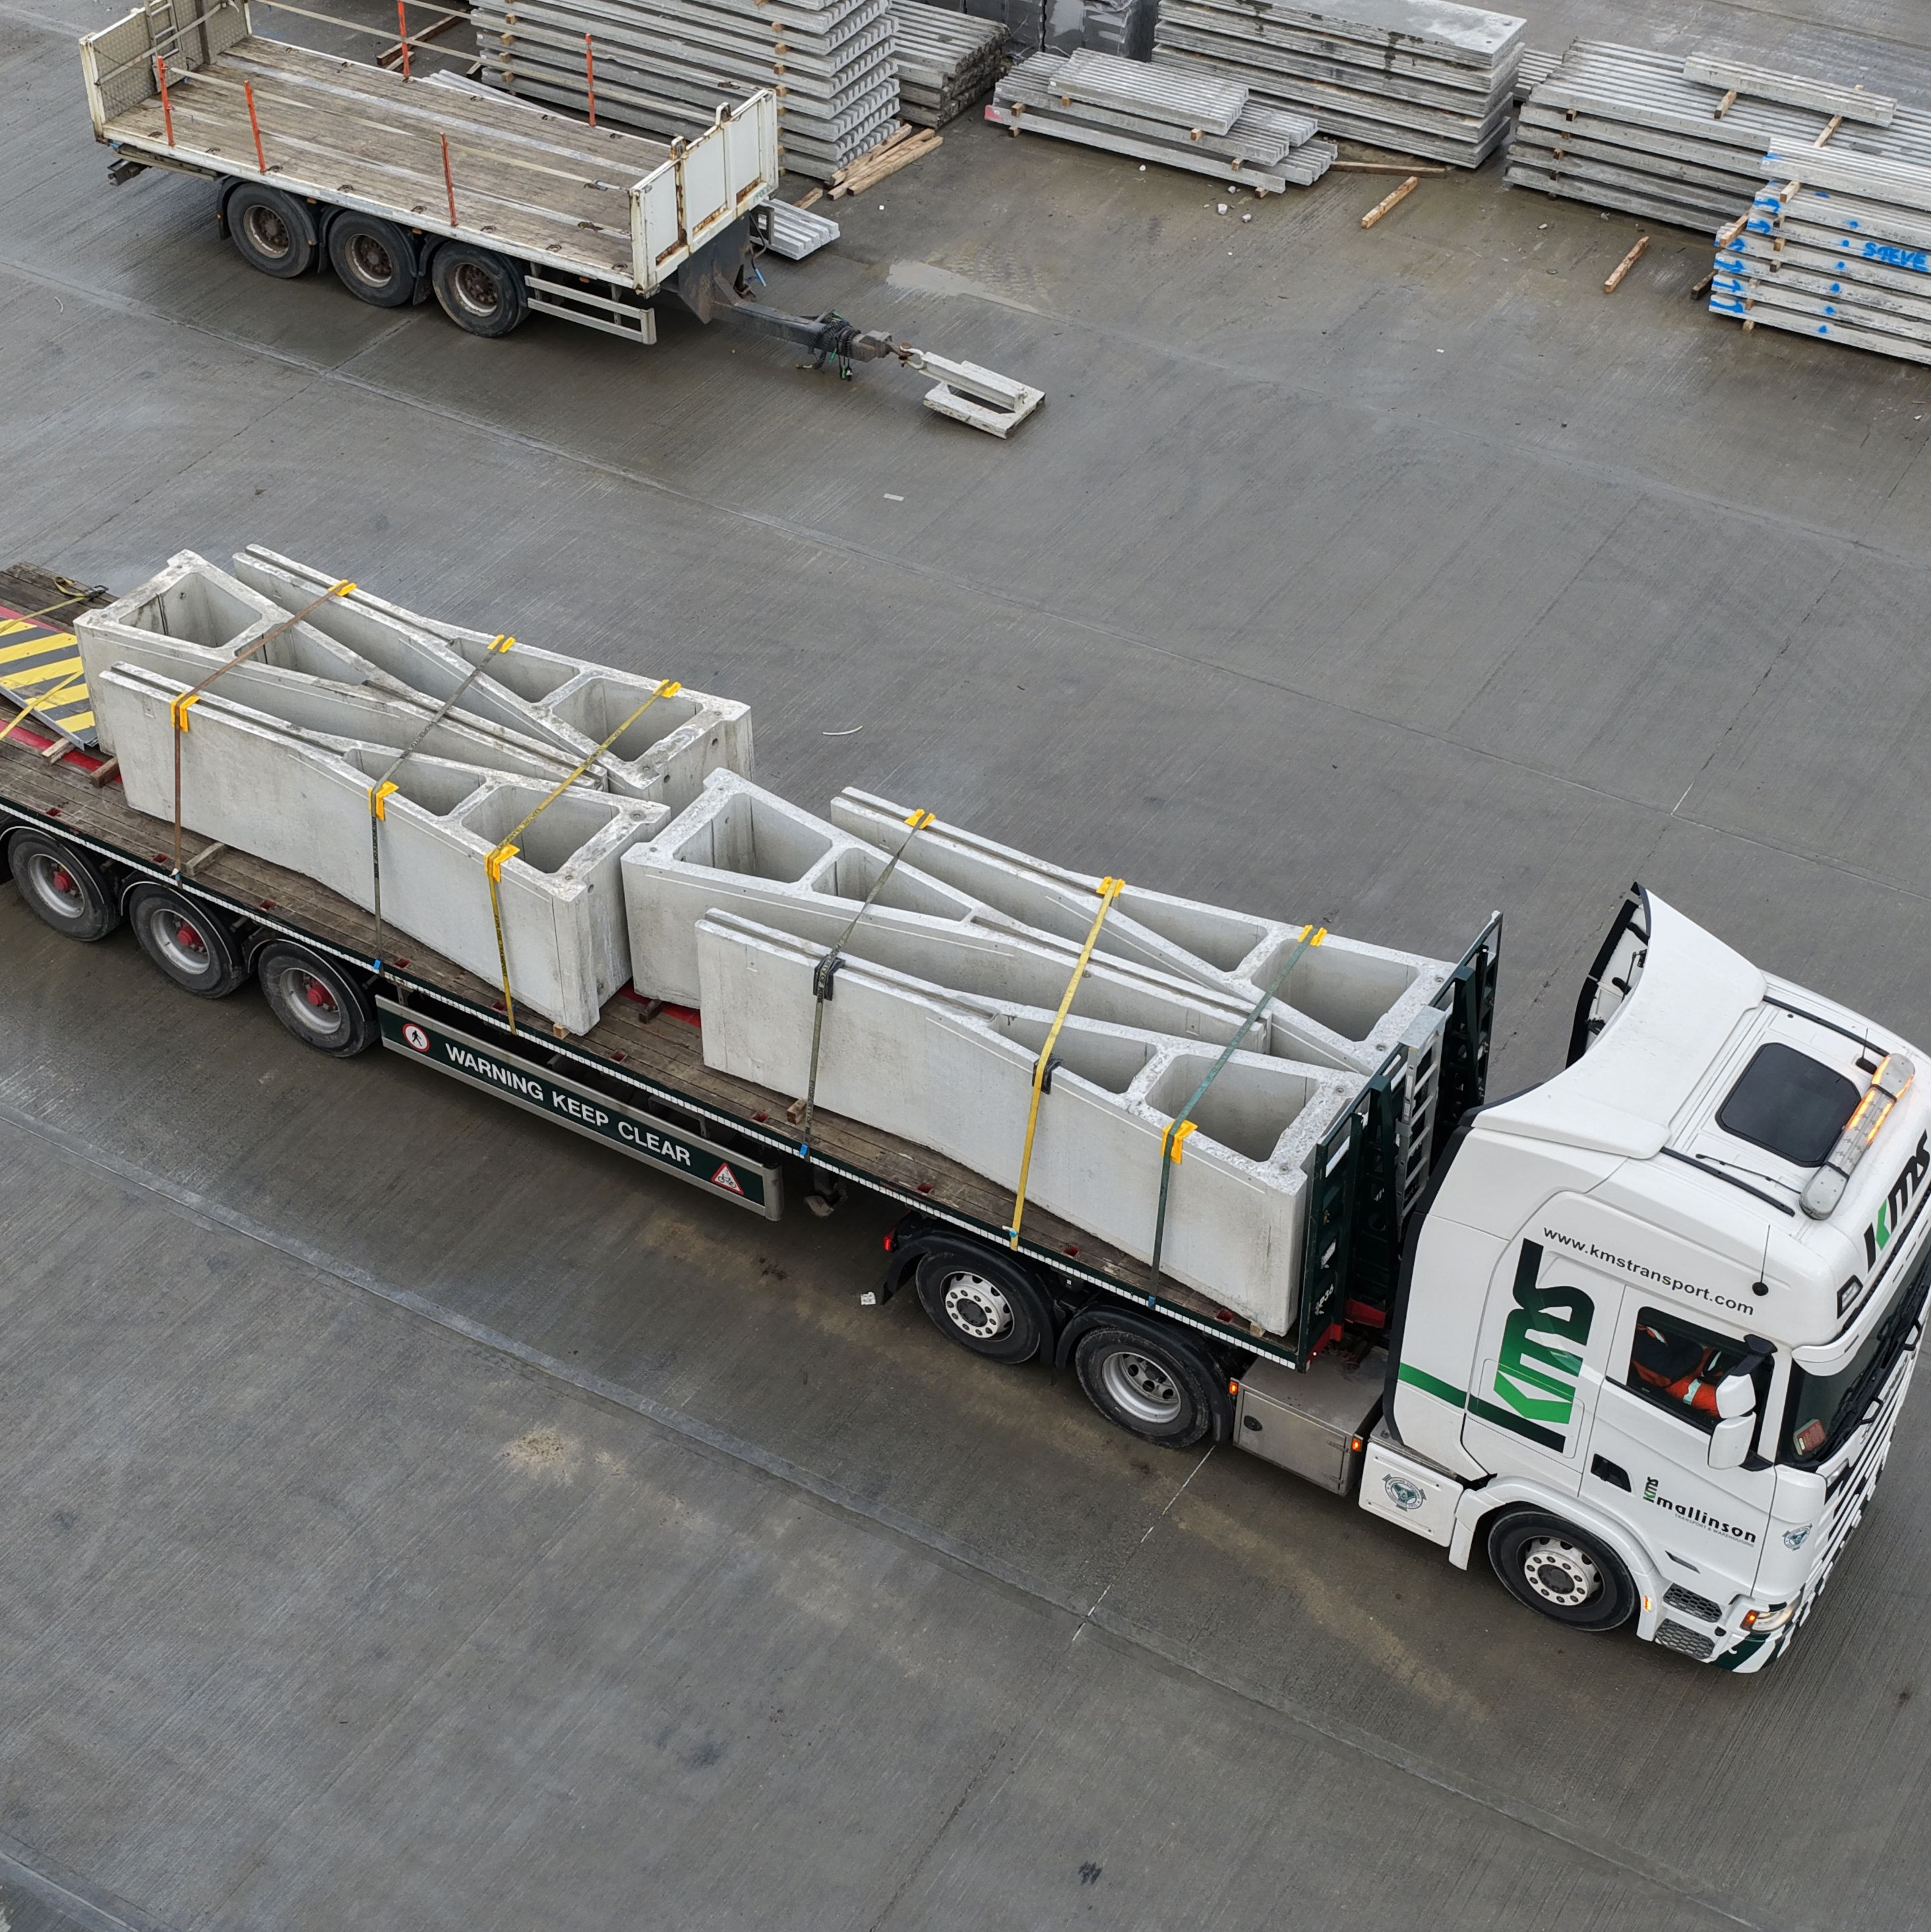
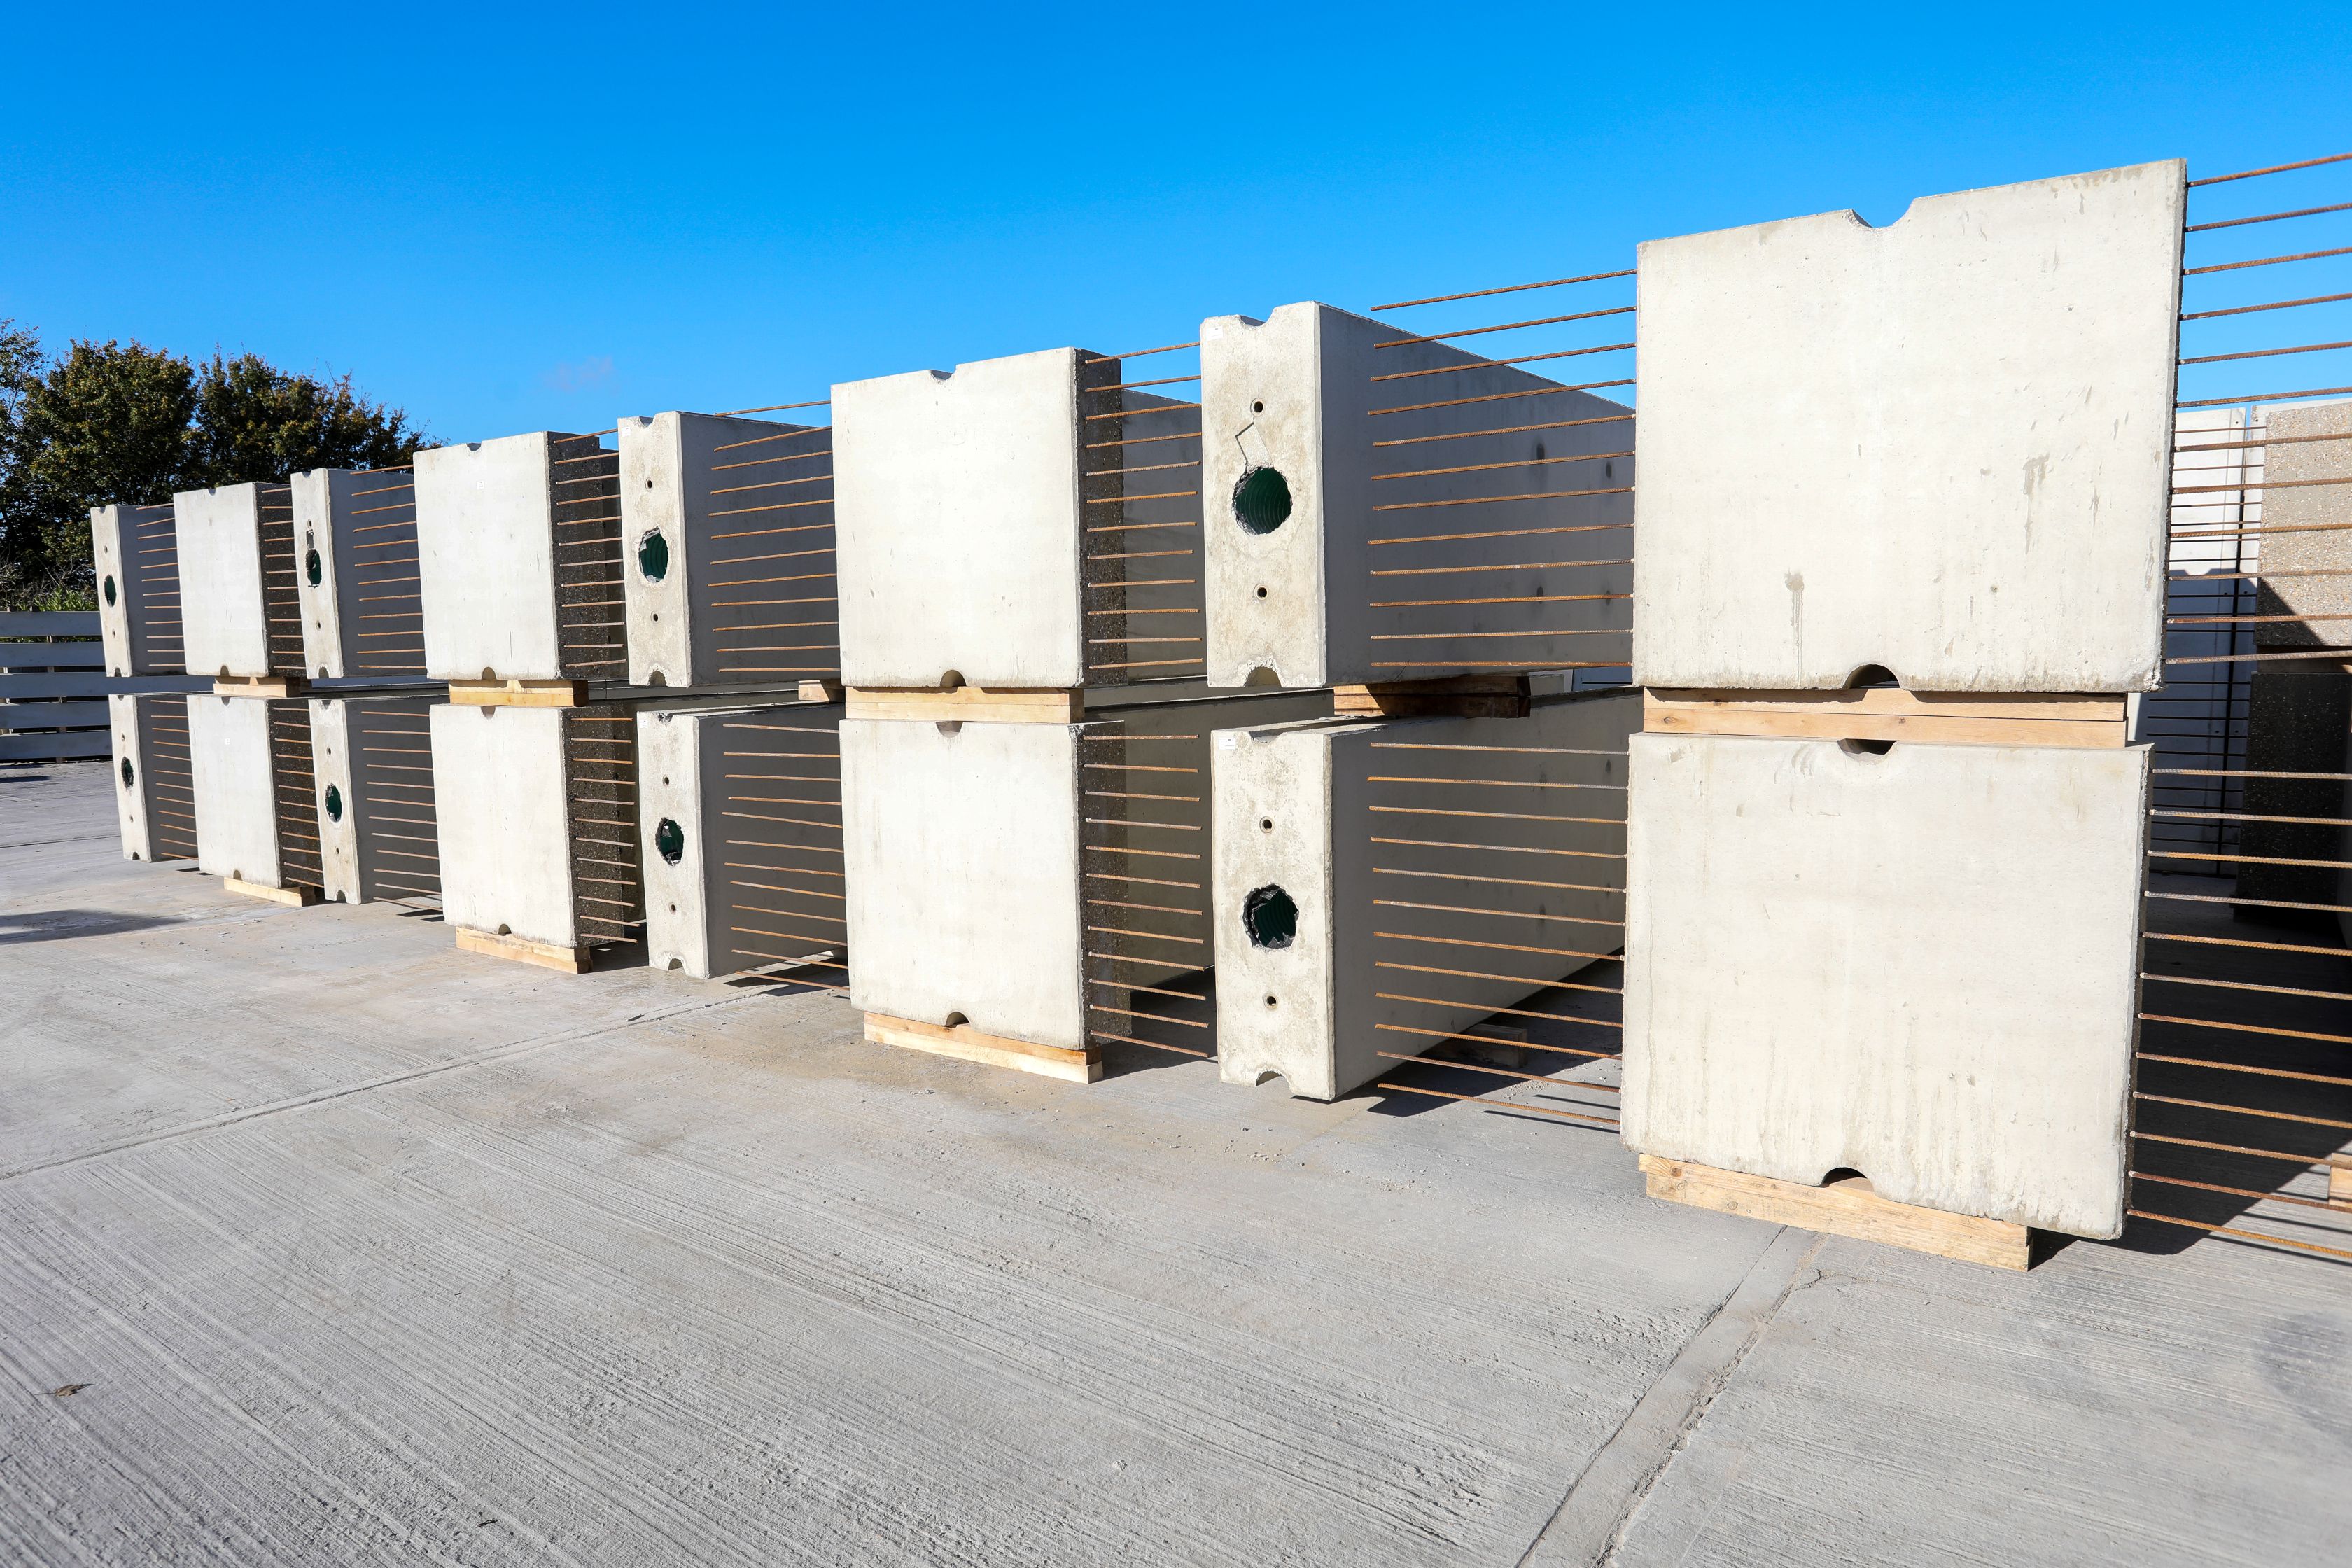
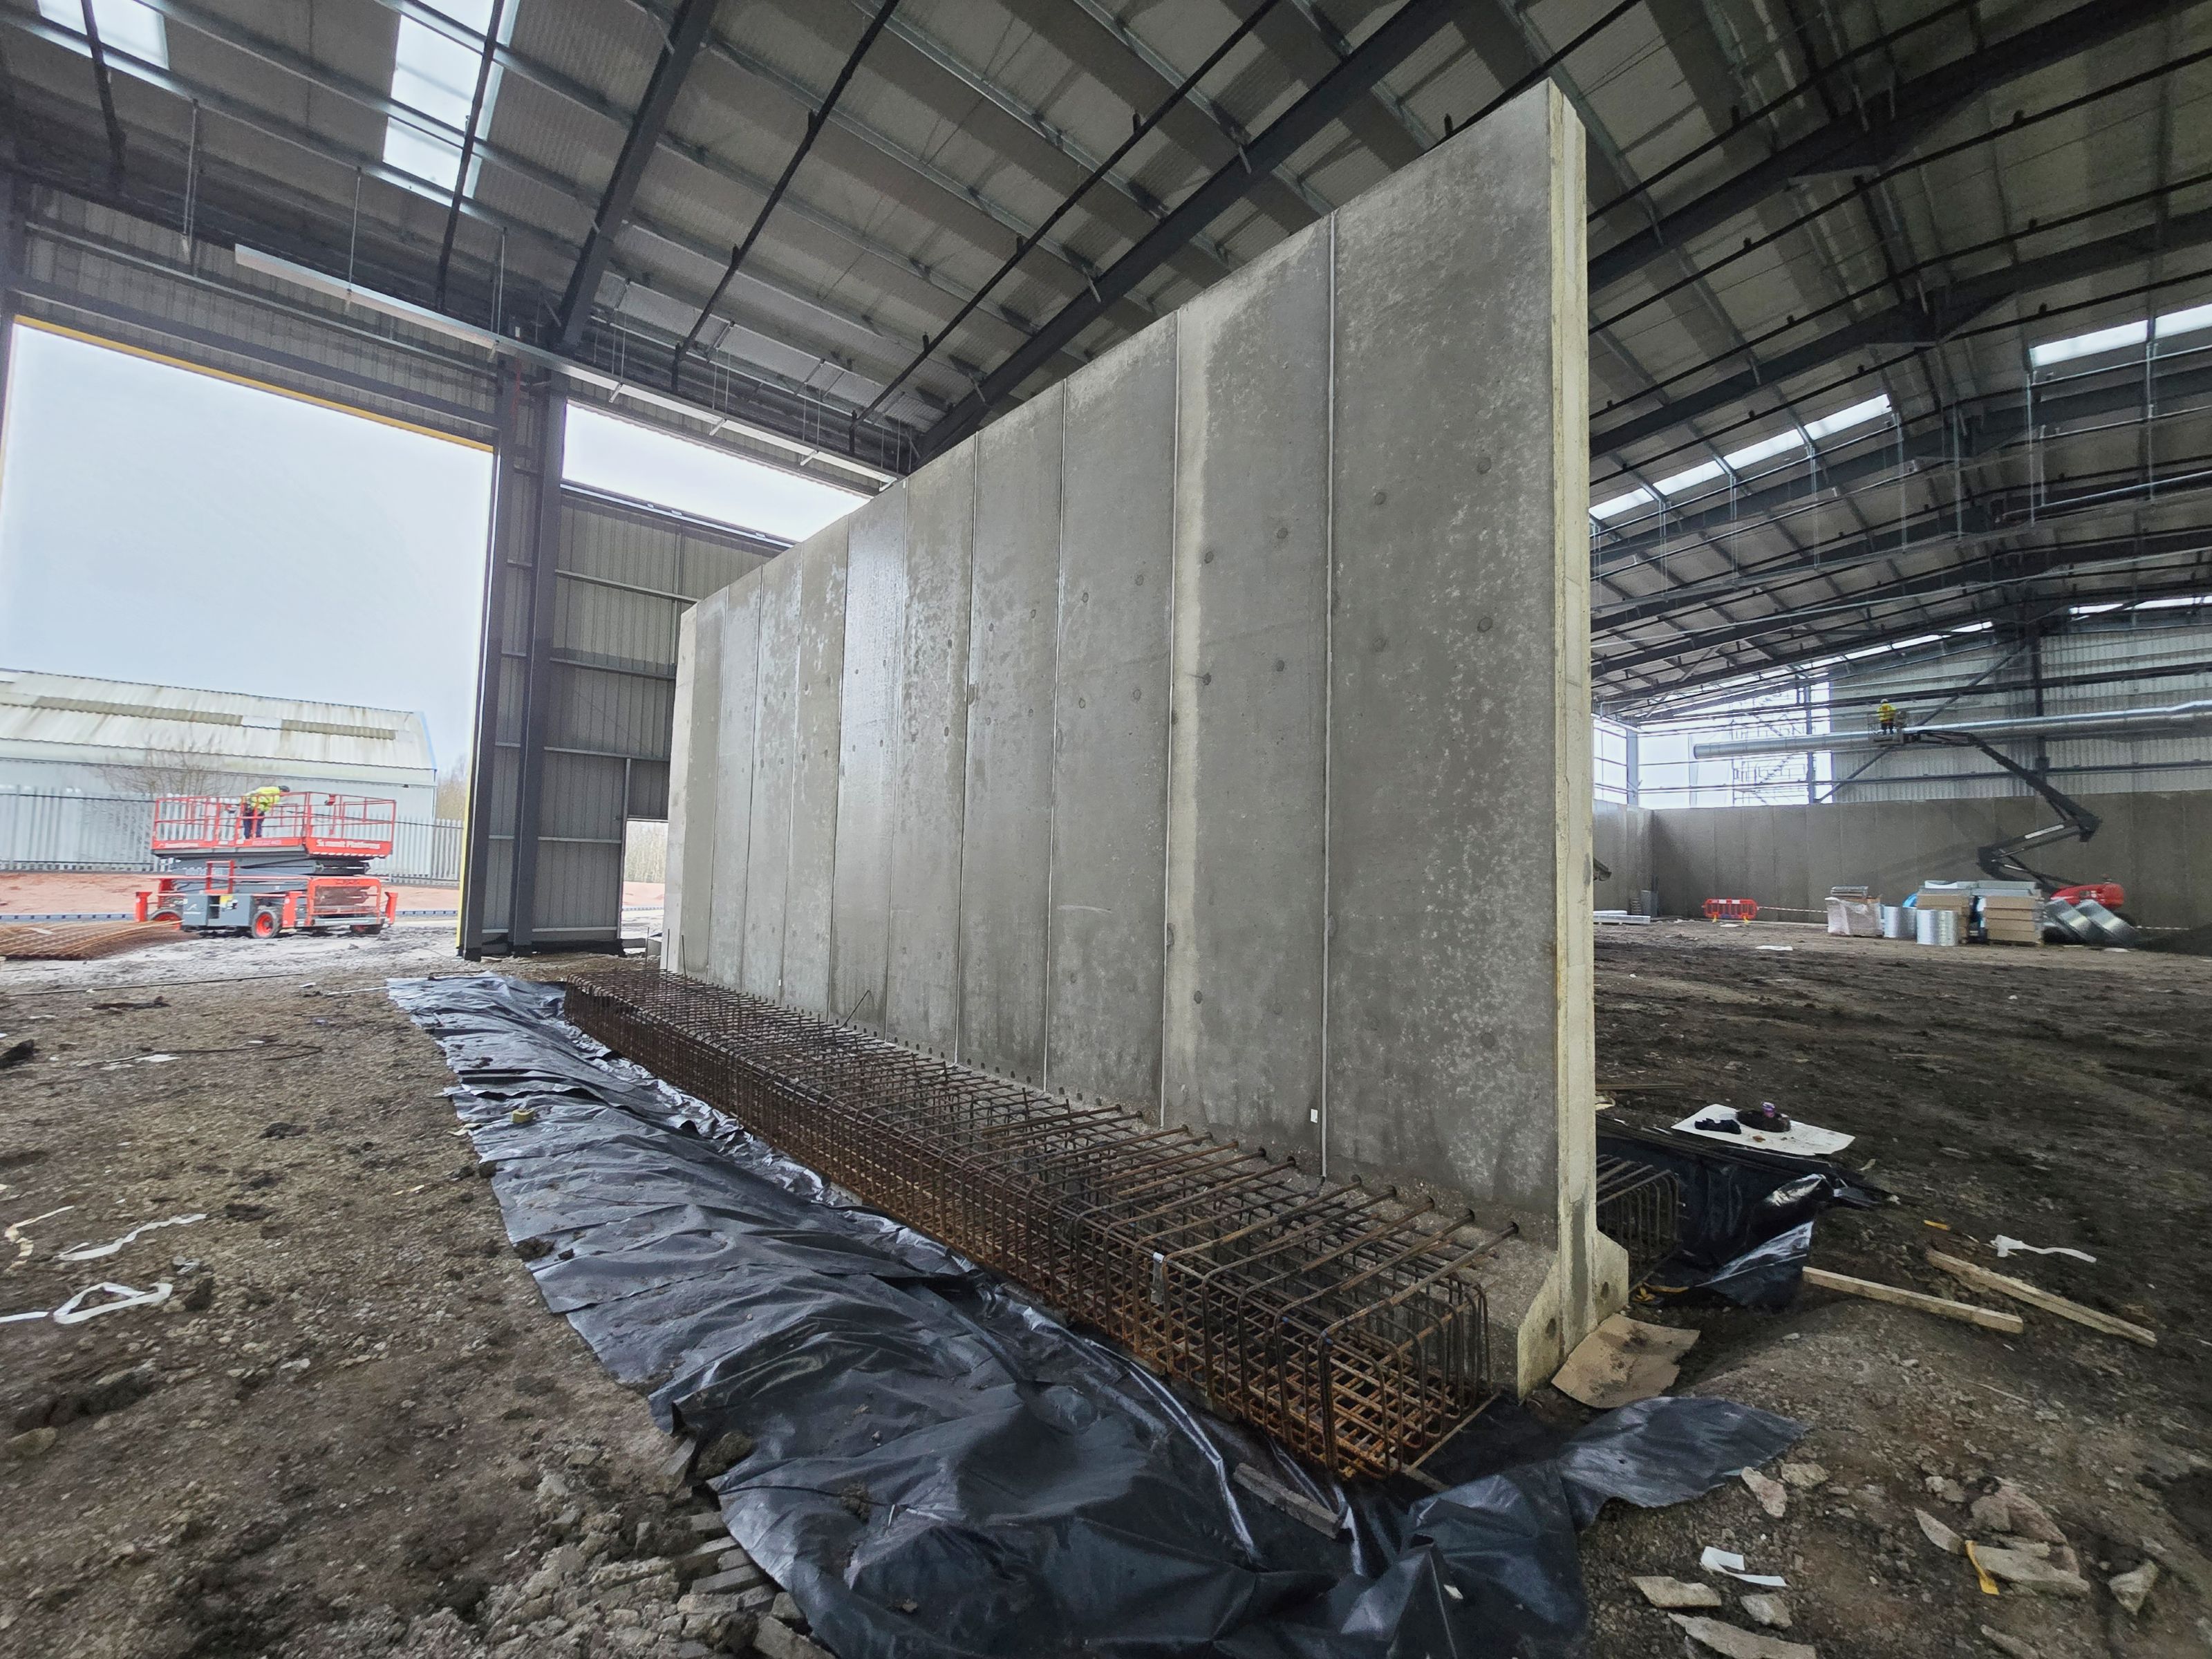
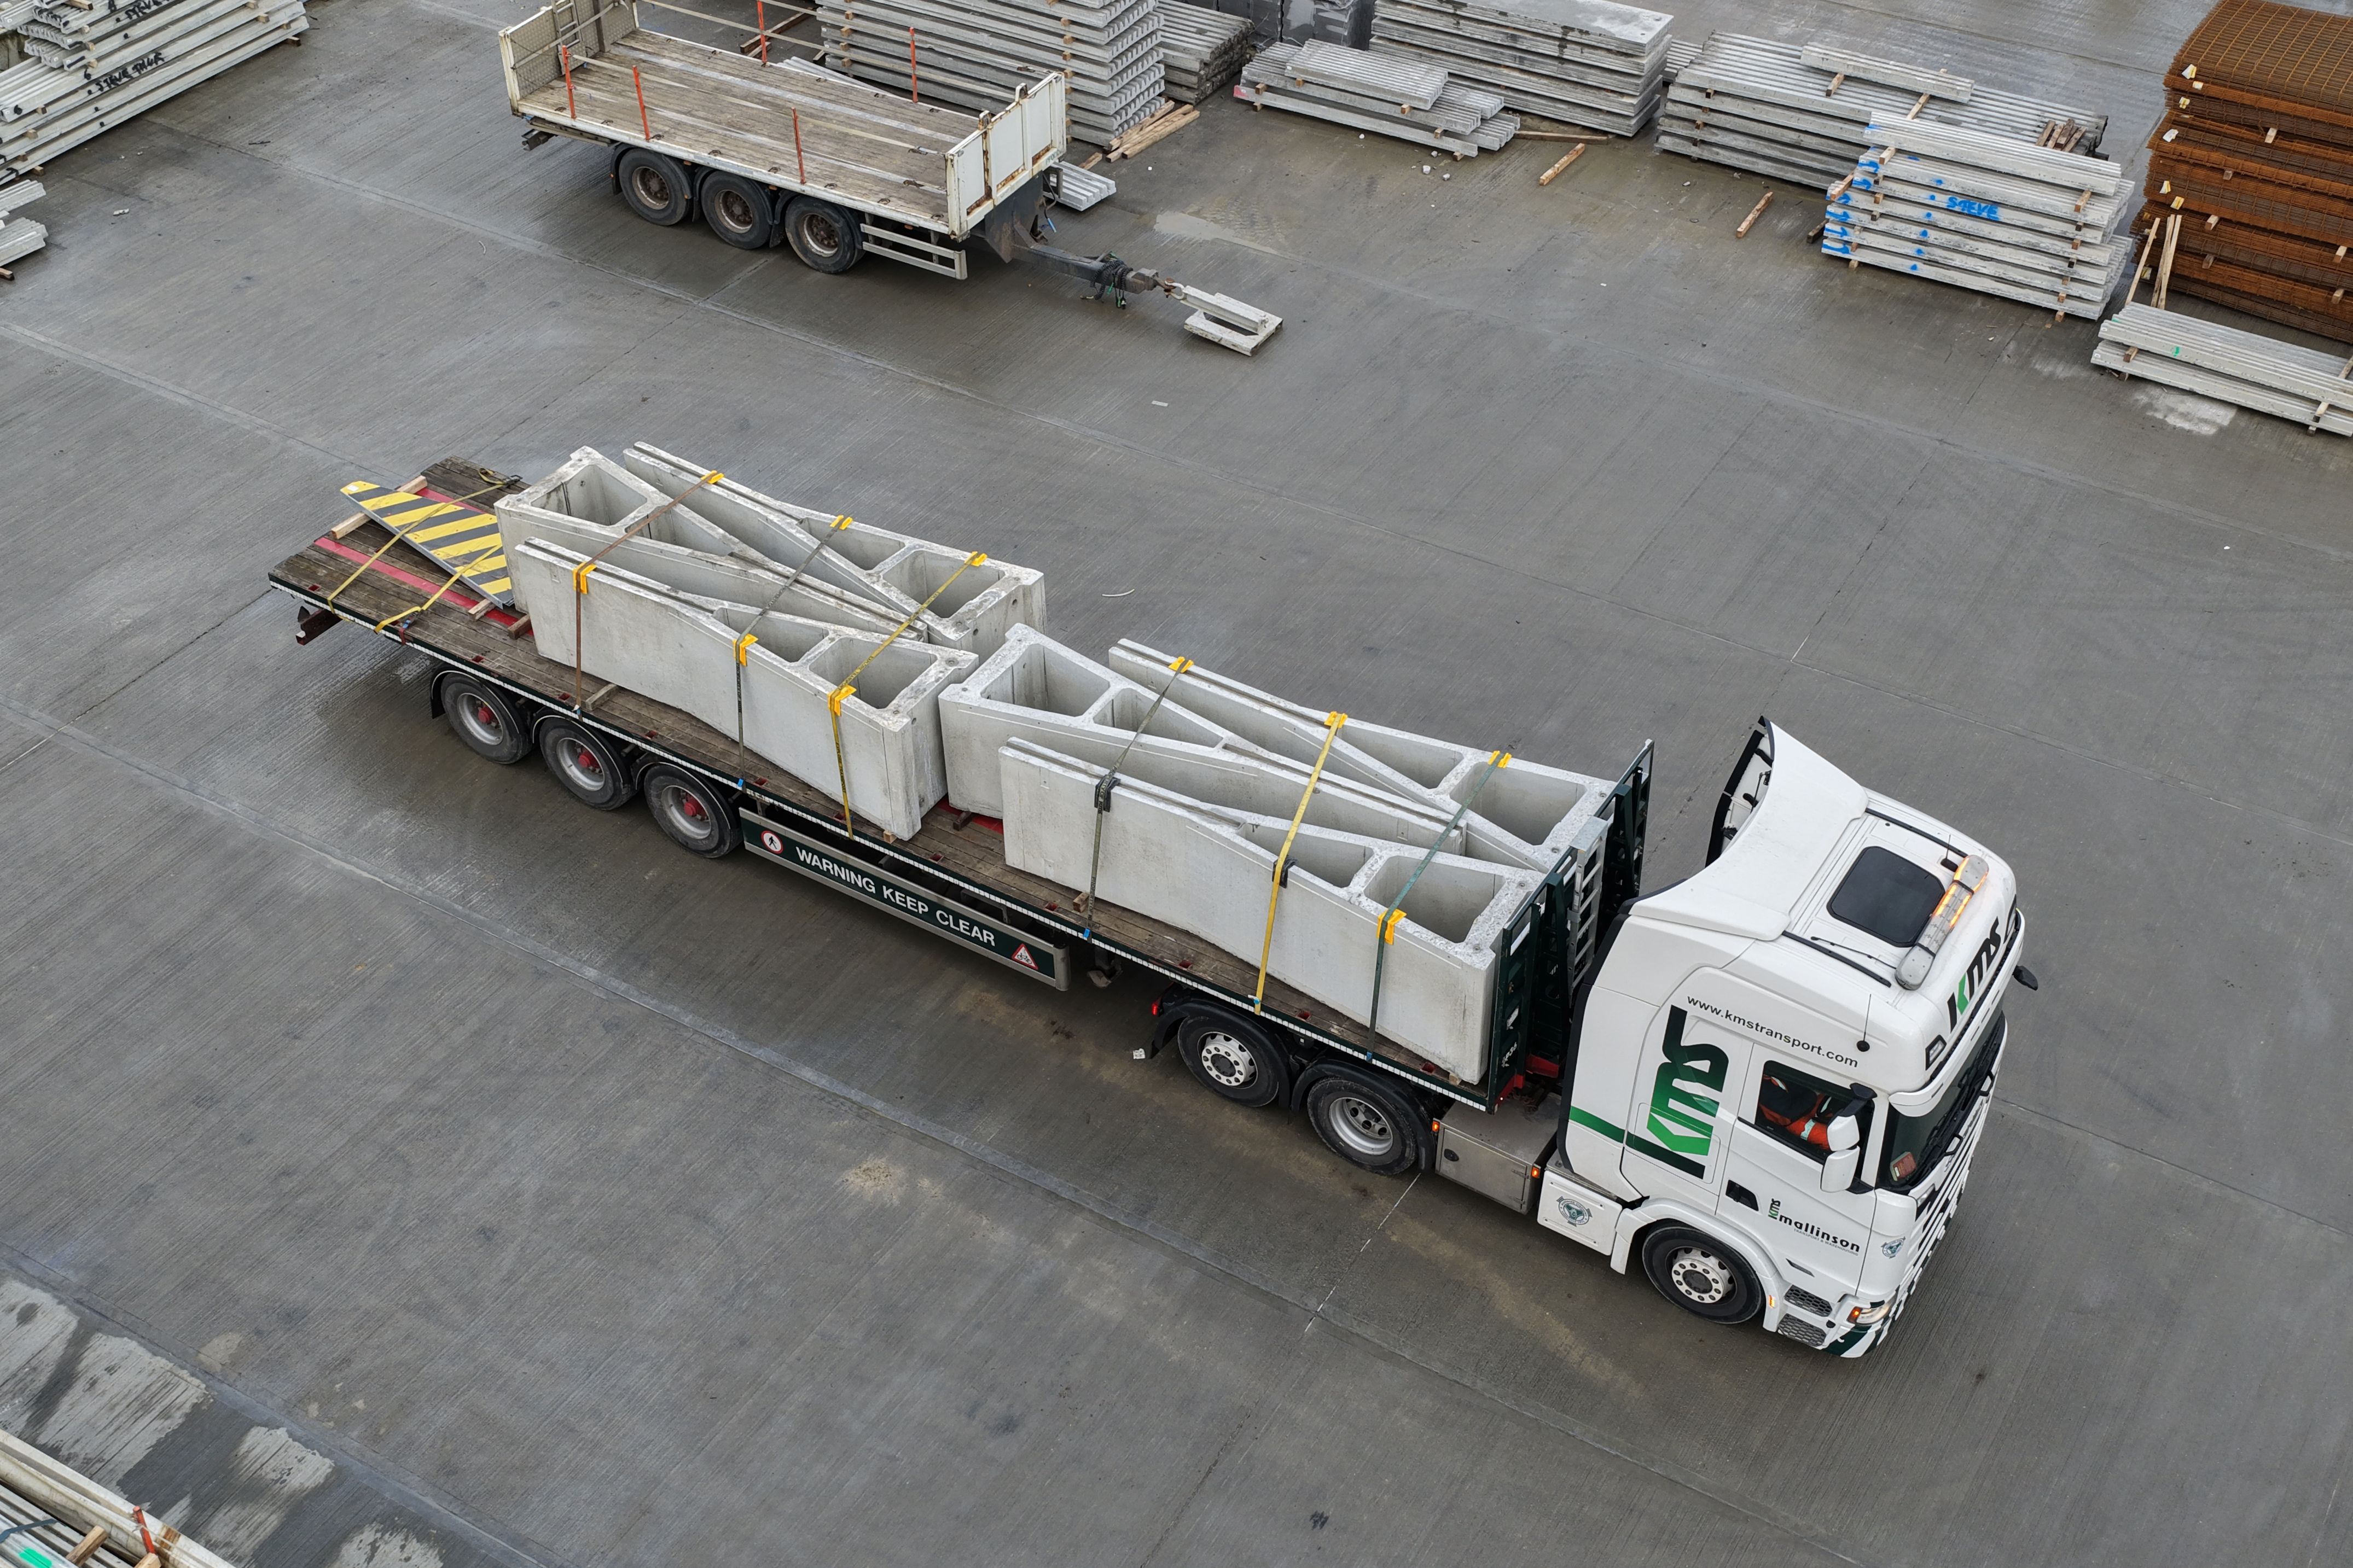
Poundfield Precast supplied and installed nearly 1,000 individual units of its high quality retaining wall products, including 236 Shuttablocs designed specifically with waste and recycling in mind. A total of 68 Alfablocs complete with steel protection plates were also supplied, along with 662 L-Blocs in three different sizes.
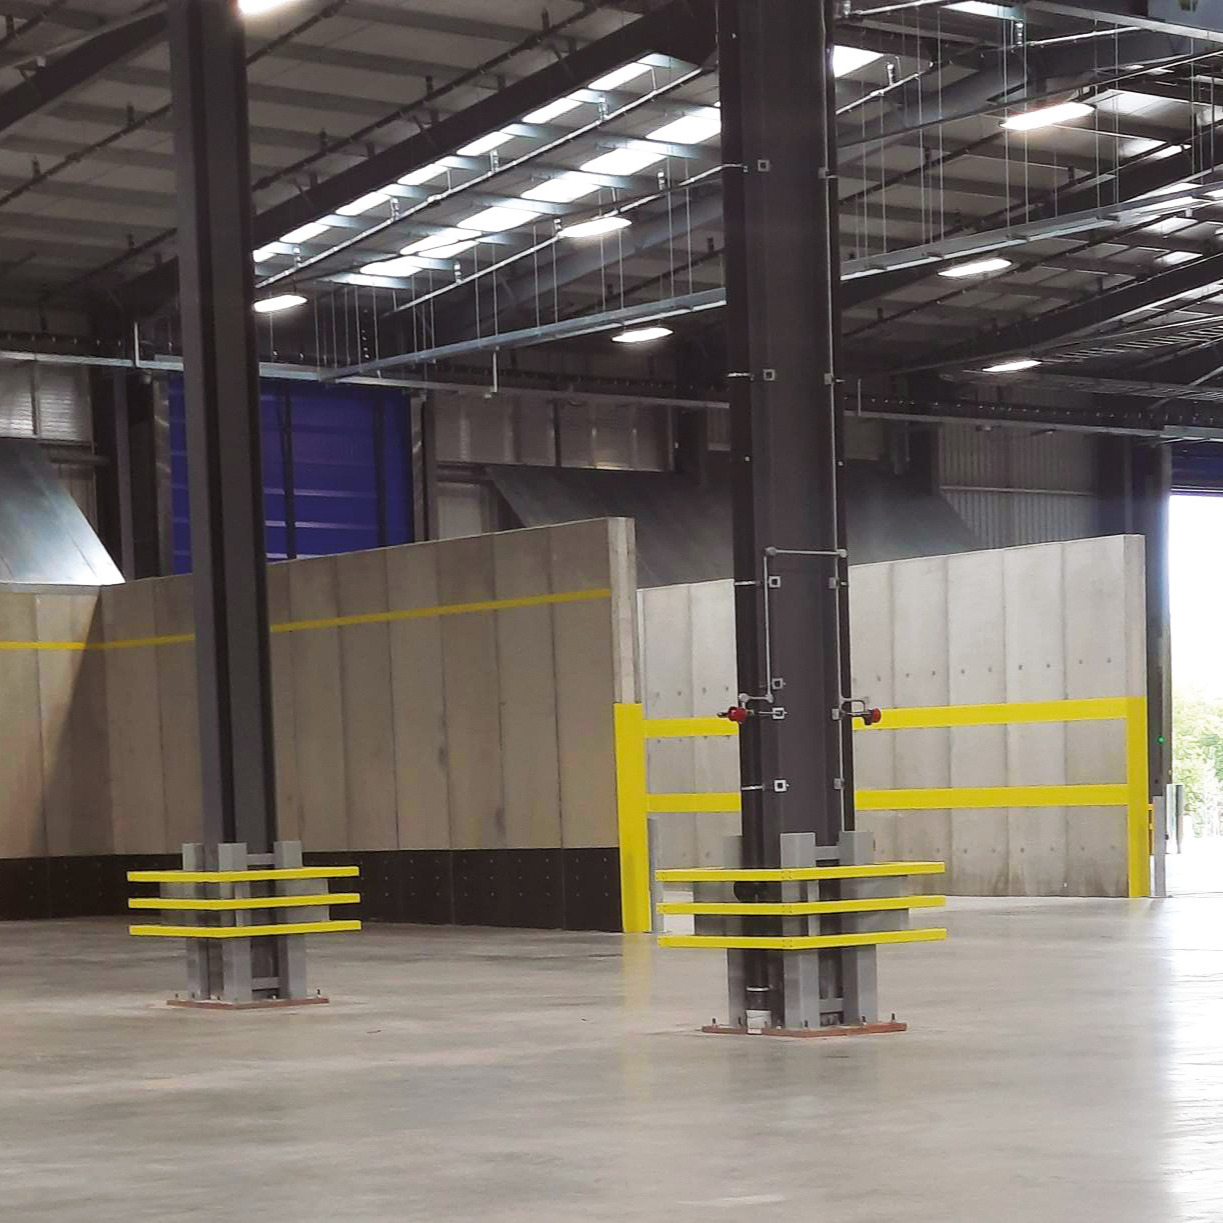
The units were used to complete a variety of projects, including creating loading bays in the waste transfer station and forming the robust storage bays, where they are helping keep recyclable materials separate to avoid cross-contamination.
Casting products with strength and durability in mind
Poundfield uses a specific concrete mix to cast its core products, which is designed to withstand difficult conditions while maintaining its strength. Each of the products used at Walsall also has its own individual advantages:
• Shuttablocs are Poundfield’s heaviest-duty system and include internal reinforcements, making the units the ideal choice where day-to-day demand on the walls is severe and a permanent, long-term system is required. The blocks incorporate a hollow core which is filled with concrete once it in position and are supplied with reinforcement in the footings, which allow them to be secured into the base.
• Alfablocs can be used as freestanding units, but in a waste and recycling environment they are usually ground fixed using bolts. They can be loaded on one or both sides and joined with steel connecting plates to form a single solid wall. This means that any load against the wall is distributed along the length of the Alfablocs rather than concentrated on a single unit, providing a heavy-duty, long-lasting solution.
• L-Blocs are interlocking, L-shaped units which use a unique tongue and groove system and can accommodate loading from either side of the wall. Easy to install, they are typically bolted down to the base to produce a solid wall.
Retaining walls in waste and recycling
Poundfield Precast’s range of specialist retaining wall products are ideal for the waste and recycling industry. As well as offering a cost-effective, quick to install solution for separating and containing waste as it moves through a plant for processing, the blocks also offer a range of other benefits.
These include:
• Robustness and durability. Poundfield products are designed to operate in tough environments, as they are able to endure everything from the wear and tear of materials being loaded and unloaded, to the corrosive impact of chemical attack from leachates on a daily basis.
• Flexibility. The Alfabloc system can offer temporary, freestanding and durable dividing walls which can be moved and reconfigured to meet changing requirements for storage. Alternatively, they can be ground fixed to provide a secure solid wall.
• Reduced fire risk. More than 300 significant fires take place at UK waste management sites every year, many of which are caused by lithium batteries mixed up in everyday rubbish. Concrete helps reduce the risk of fire spreading and – depending how it is installed – can create a two-hour firewall which gives the fire service valuable time to contain the blaze and prevent it’s spread.
Delivering on time and on budget
Using Poundfield’s unique retaining wall products during the construction of the Walsall household waste recycling centre and transfer station helped make sure the project was finished on time and to budget. The quality and strength of the materials Poundfield supplied will also support the facility’s longevity, ensuring it continues to provide residents with modern, easy-to-use recycling facilities for many years to come.
For more information about any of Poundfield Precast’s retaining wall products and the benefits they bring across a range of industries, visit www.poundfield.com, call 01449 723 150 or email enquiries@poundfield.com
Boosting sustainability at Europe’s largest recycling centre
| T | (01449) 723150 |
|---|---|
| E | enquiries@poundfield.com |
| W | Visit Poundfield Precast's website |
| The Grove, Creeting St Peter, Ipswich, IP6 8QG |
Products by this Company